Food Packaging Ink Adhesive Compliance: Records
Build an auditable evidence chain from the finished package and intended use back to the exact ink, coating, adhesive, substrate, process, and production lot.
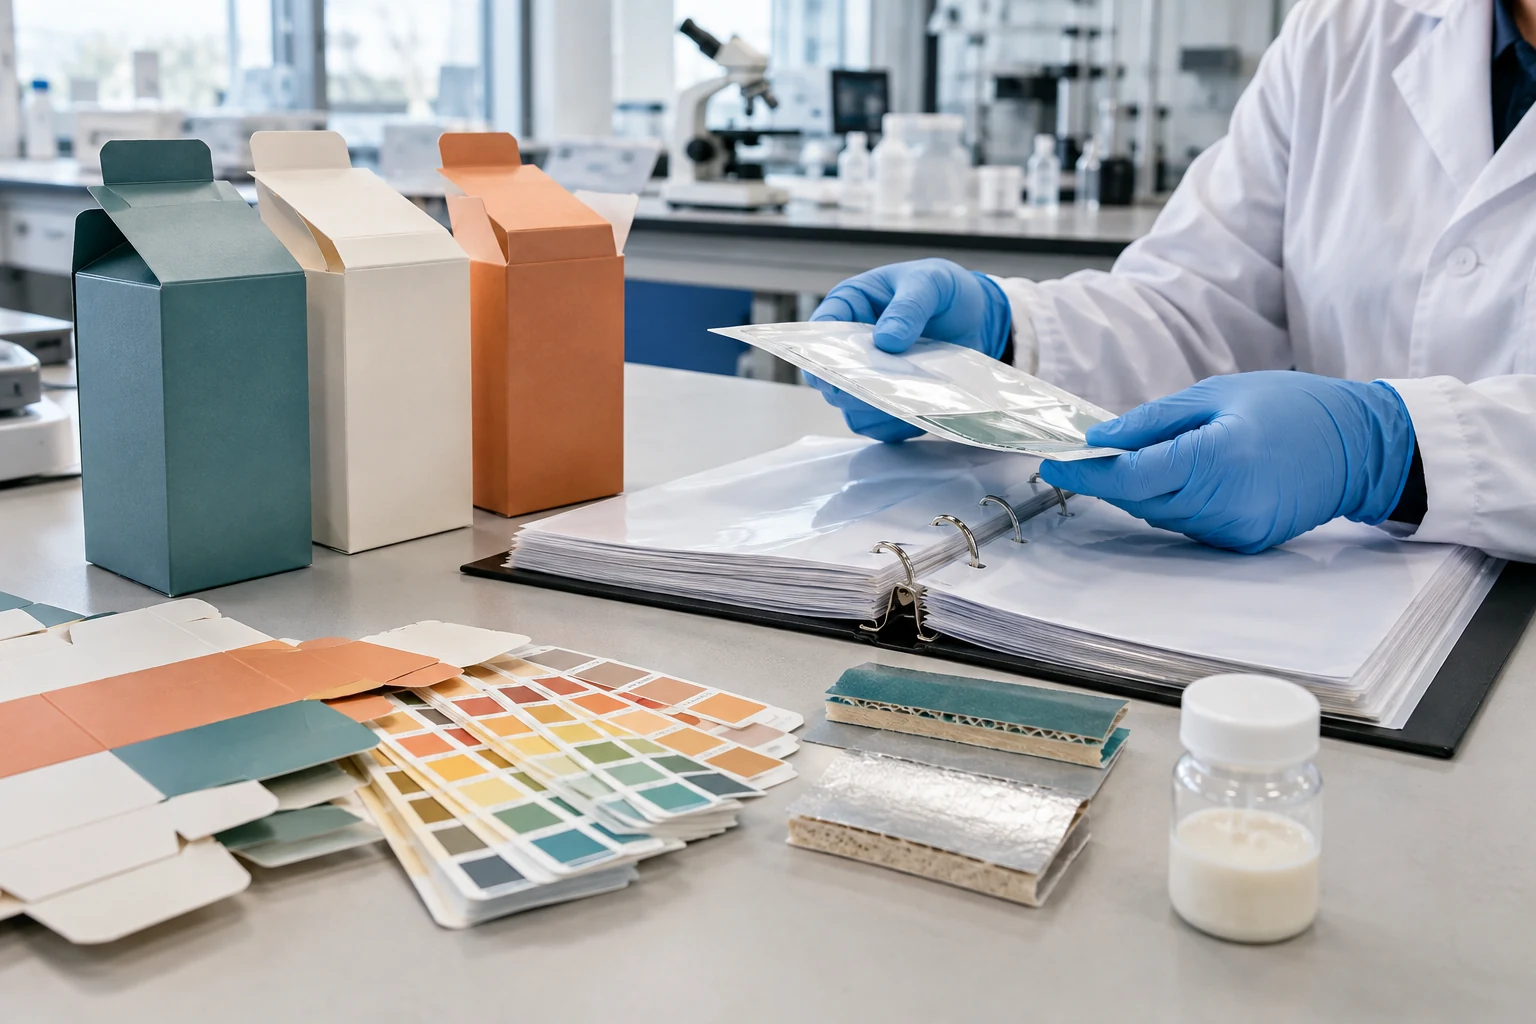
food packaging ink adhesive compliance is supported by a connected record set, not one universal certificate. Buyers should collect the finished-pack specification, bill of materials, ink and adhesive product identities, supplier declarations, applicable regulatory status, restrictions of use, migration or risk-assessment rationale, print and bonding process controls, production traceability, and documented change approval.
The record set must match the real package: substrate, printed side, ink coverage, varnish or coating, adhesive location, food type, contact route, temperature, time, storage, stacking, and market. A declaration that cannot be tied to the production-intent structure and lot is weak evidence even when it carries an official-looking heading.
This guide is a procurement framework for private-label tableware packaging and related food-contact applications. It does not decide legal compliance for a particular market; the buyer, packaging converter, material suppliers, testing laboratory, and qualified compliance adviser must confirm the applicable rules and evidence for the finished article.
Buyer Answer: Build Evidence in Five Connected Layers
First identify the complete package and foreseeable food-contact pathway. Then link every ink, coating, primer, overprint varnish, laminating adhesive, cold seal, label adhesive, and carton glue to a controlled product code, supplier, revision, intended-use statement, and restriction.
Next document why transfer is controlled through formulation, barriers, set-off prevention, curing or drying, application conditions, and—where appropriate—migration testing or a qualified risk assessment. Finally retain lot traceability, inspection records, and a change-control gate so approved evidence still describes what the factory actually used.
Define the Finished Package and the Real Transfer Path
Begin with a construction drawing or specification that names every layer in order. Record the food-facing substrate, any barrier or lamination, printed surface, primer, ink series, varnish, adhesive, label, closure, and secondary component that can affect transfer. Include thickness, basis weight, surface treatment, print process, coverage, adhesive coat weight or application range, and the supplier product codes used for approval.
Separate direct contact, indirect contact, and no-intended-contact claims. An ink printed on the outside of a carton may still transfer through a porous substrate, enter the headspace, or set off onto a food-facing surface when sheets, labels, or webs are stacked or wound. An adhesive can sit behind a functional barrier, at a seam near an opening, or under a label on primary packaging; those positions create different exposure questions.
Describe the food and conditions of use with enough precision to choose evidence. Dry cereal at ambient temperature, fatty confectionery, hot-filled sauce, chilled dairy, frozen food, and a tableware gift set with no unpackaged food exposure are not interchangeable scenarios. State contact time, temperature, shelf life, heating, freezing, repeated use, and whether the consumer can reasonably misuse the package.
Map the converting process because chemistry alone does not define the finished result. Printing speed, lamp output, dryer settings, mix ratio, viscosity, residual solvent control, adhesive application weight, curing time, reel tension, stacking pressure, and storage time can affect transfer or bond performance. The approved window should be measurable on the production line.
Photographs and a dieline help reviewers locate print and glue, but they do not replace the controlled specification. Assign the construction a revision number and connect it to the artwork, color standard, packaging sample, bill of materials, test plan, and order. This makes later comparison possible when a supplier proposes an apparently minor substitution.
For tableware programs, use the packaging quotation requirements guide to collect dimensions, quantities, artwork versions, carton hierarchy, and channels before the evidence review starts. The compliance file should describe the same commercial configuration that was quoted.
A compliance file begins with intended use
Without the actual contact pathway and conditions, a supplier can only provide broad product information. Buyers should reject conclusions that silently assume a barrier, low temperature, short contact, or non-fatty food when the approved package says otherwise.
Ask who owns the final assessment at each level: raw-material maker, ink or adhesive formulator, converter, packer, brand owner, and importer. Responsibilities can differ by contract and market, but the handoffs should never be left implicit.
Collect Product Identity, Composition Statements, and Supplier Declarations
Request the current technical data sheet and safety data sheet for each ink, additive, varnish, primer, adhesive, hardener, cleaner with possible carryover, and processing aid relevant to the package. Record the trade name, product code, manufacturer, manufacturing site when material, document version, issue date, color or component, and approved supplier. A family statement is insufficient if individual colors or adhesive components have different restrictions.
The safety data sheet supports hazard communication, but it is not a food-contact authorization or migration assessment. Conversely, a declaration of compliance or statement of composition may address food-contact use without describing safe handling. Keep the documents together while preserving their different purposes.
Supplier declarations should state the intended application, applicable regulatory basis or industry guidance, known restrictions, maximum use level or coat weight where relevant, excluded food types or conditions, barrier assumptions, and any substances requiring downstream assessment. They should also explain whether the conclusion applies to the wet product, properly cured print, finished laminate, or another defined state.
For formulations treated as confidential, request disclosure through an agreed channel to a competent laboratory or regulatory reviewer. A generic phrase such as “food grade” does not identify the legal basis, exposure limit, purity requirement, or evaluated use. Procurement can protect confidential information without accepting an unreviewable claim.
Track pigments and each spot color as well as the base ink system. Color matching can introduce a new concentrate, additive, or mixing ratio after the generic series was approved. Metallic, fluorescent, opaque white, low-migration, UV/EB-cured, water-based, solvent-based, and conventional offset systems can have distinct process and assessment needs.
Adhesive records should distinguish structural lamination, heat seal, cold seal, pressure-sensitive label, tape, carton side seam, window patch, and temporary fixation. Ask whether the product code and conditions match the actual substrate pair, application amount, cure, food separation, and temperature. A carton glue declaration cannot automatically support a flexible-laminate adhesive.
Control the exact commercial products
Create an approved-material register with one row per product code and a link to the supporting document revision. Include expiry or review dates, approved sites, allowed applications, and the package constructions that use the material.
When documents contain caveats, convert them into purchase-order and production controls. A restriction that remains buried in a PDF is unlikely to prevent the wrong ink, hardener ratio, or cure time on the factory floor.
Evaluate Migration, Set-Off, Barrier, and NIAS Evidence
Migration evidence should answer a defined question about the finished package. The plan may use testing, modeling, compositional review, worst-case calculation, functional-barrier reasoning, or a documented combination, depending on the legal framework and exposure scenario. Record why the chosen approach is suitable and which uncertainties remain.
For printed materials, review both through-substrate migration and set-off. Set-off can occur when the printed outside touches the food-facing inside during reel winding, sheet stacking, blank storage, or nested package handling. Controls may include ink selection, drying or curing verification, stacking conditions, interleaving, winding tension, storage time, and a process design that prevents relevant contact.
Functional-barrier claims require evidence for the actual barrier material, thickness, integrity, temperature, time, food, and substances under review. A layer that limits one compound under one condition is not automatically an absolute barrier for every ink or adhesive constituent. Seams, pinholes, cut edges, windows, and process damage may also bypass the nominal structure.
Non-intentionally added substances can arise from impurities, reaction products, degradation, curing, residual solvents, contaminants, and interactions between materials. Ask suppliers what screening or risk-assessment information they can share, what is intentionally covered by their declaration, and what remains for the converter or finished-package assessment. Avoid interpreting a positive list as proof that every possible NIAS has been evaluated.
Testing reports should identify the sample, construction, artwork or coverage, production process, conditioning, simulant or food, time, temperature, analytical method, reporting limit, substances sought, results, specification, and conclusion. Confirm laboratory competence and whether the method and detection limits can address the relevant restriction. A report on a different substrate or lightly printed sample may not represent the approved pack.
If a worst-case calculation is used, retain the formula, inputs, assumptions, surface-area-to-food ratio, ink or adhesive mass, substance concentration, transfer fraction, and applicable limit. Conservative assumptions can efficiently screen low-risk cases, but unexplained numbers are not auditable. Escalate when missing composition or uncertain exposure prevents a defensible conclusion.
Evidence must bridge formulation and finished use
A supplier statement can support the input-material layer while the converter demonstrates controlled application and the brand owner confirms the finished use. The chain fails when one party assumes another has assessed set-off, curing, actual coverage, or consumer conditions.
The food-contact traceability guide shows how to connect declarations, test reports, specifications, and lots. Apply the same discipline to the printed package and its converting inputs.
Turn Restrictions into Printing and Bonding Process Controls
Translate the evidence file into a job instruction before production. The instruction should lock the substrate treatment, ink and adhesive product codes, mixing ratios, additive limits, print sequence, coverage or anilox specification, dryer or cure settings, line speed, coat weight, nip or sealing conditions, and minimum cure or hold time. Record permitted adjustment and who can authorize it.
Incoming control verifies identity, condition, lot, shelf life, packaging integrity, and document status. Segregate obsolete, expired, unapproved, or trial materials. Barcode or batch scanning can reduce selection errors, but the master data must still distinguish similarly named grades and color variants.
During printing, monitor parameters linked to the approved window. Depending on the process, this may include viscosity, pH, temperature, solvent balance, UV dose, lamp status, line speed, residual solvent, rub resistance, odor, or cure indicators. Define measurement frequency, instrument control, response limits, and disposition when a reading fails.
Adhesive preparation and application need equivalent discipline. Verify component ratio, mixing, pot life, viscosity, coat weight, open time, temperature, pressure, bond location, cure time, and environmental conditions as applicable. Retain start-up and restart samples because a stable reading later in the run does not prove the first units were acceptable.
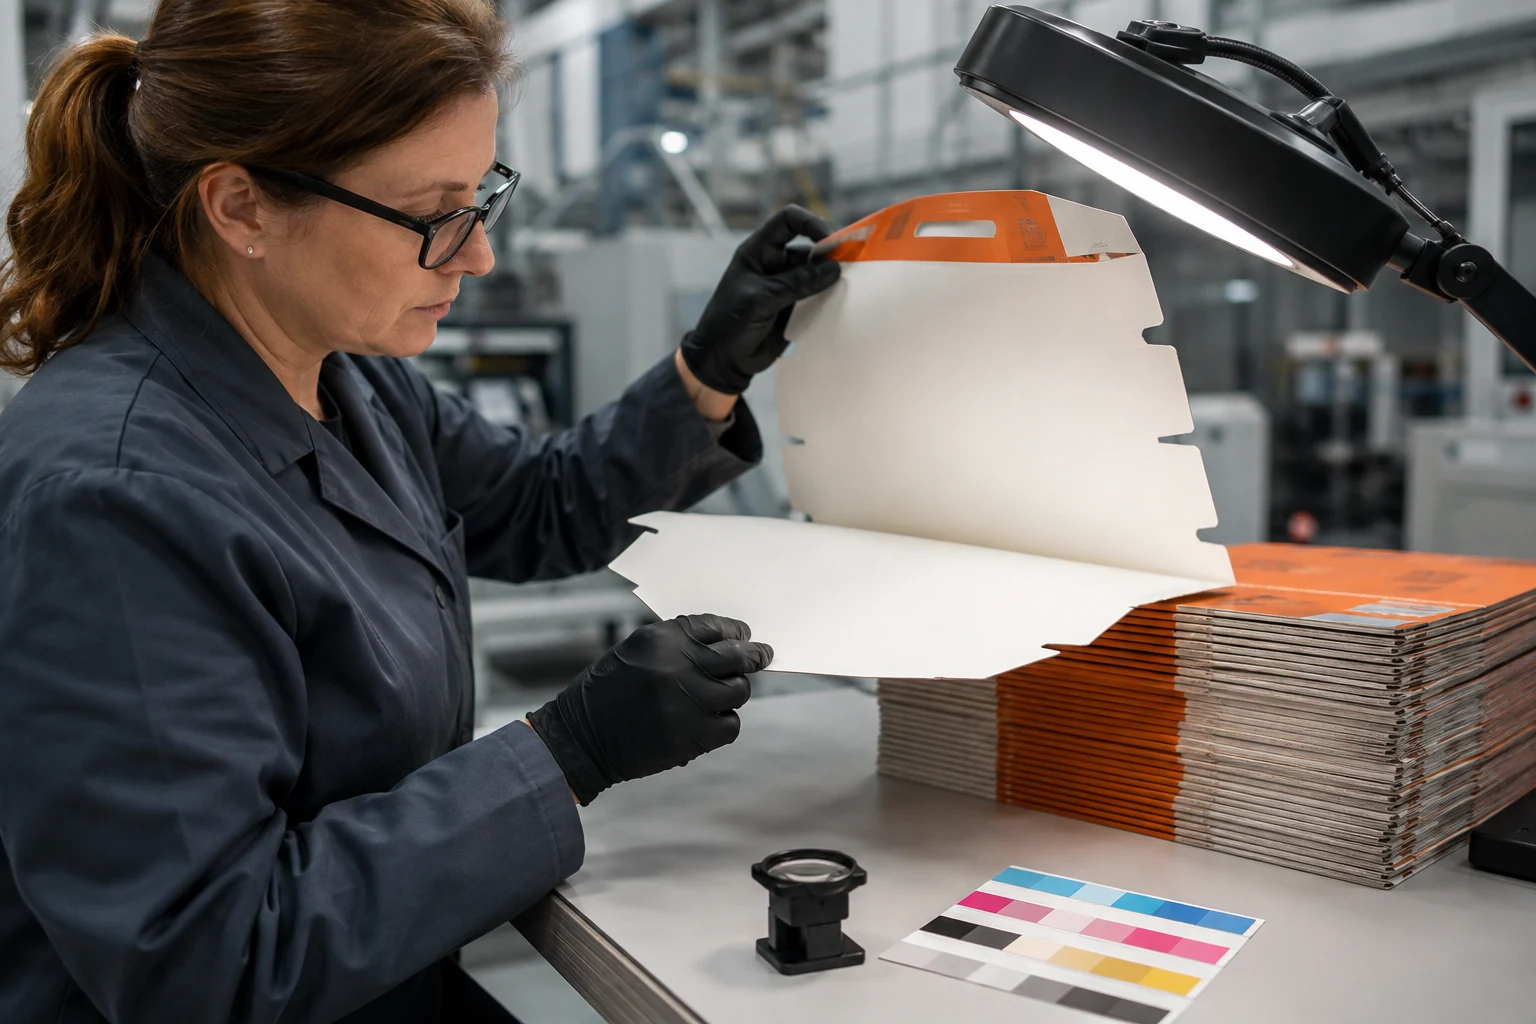
Finished-pack inspection should include registration, color, abrasion, odor or sensory concerns where appropriate, blocking, set-off signs, seam placement, squeeze-out, delamination, label lift, opening performance, contamination, and barcode readability. These checks do not replace chemical assessment, but they reveal process departures that can invalidate its assumptions.
Buyers can send the package construction and intended-use brief for an evidence-gap review. The review should identify missing links before the production sample is approved, not after a shipment has been packed.
A restriction is useful only when production can observe it
Write acceptance limits in units the line and quality team can measure. Define the validated indicators, time, and conditions when compliance depends on complete curing. Do not rely on an instruction that only says to ensure full cure.
Link deviations to quarantine, investigation, rework limits, retesting, and customer notification rules. A batch should not regain approved status through an undocumented judgment.
Verify Traceability, Sample Identity, and Change Control
The production record should connect the purchase order and packaging SKU to the finished-pack lot, converter job, date, machine, shift, substrate lot, every ink and additive lot, adhesive components, mixing records, process checks, inspection results, retained sample, and shipment. This is the minimum path for investigating a complaint or regulatory query without guessing which inputs were used.
Retained samples should represent the approved construction and production lot. Store them under defined conditions for an appropriate period, label both printed and food-facing sides, and preserve enough material for visual, bond, and analytical follow-up. Keep a signed or digitally controlled approval sample separate from casual sales samples.
Change control must cover more than a new trade name. Supplier site, raw-material source, formulation, pigment, additive, substrate coating, recycled content, thickness, print process, anilox or coverage, adhesive coat weight, cure, artwork, package geometry, food, shelf life, storage, market, and distributor can alter the assessment. Define which changes require notification, document refresh, sample review, or testing.
Set periodic document review rather than assuming declarations remain current forever. Regulatory lists, supplier formulations, company names, manufacturing sites, standards, and guidance can change. The register should flag superseded files and prevent a purchasing system from calling an obsolete product approved.
Audit a traceability challenge by selecting one finished lot and retrieving the input lots, declarations, process records, inspection evidence, approval sample, and shipment within a target time. Then reverse the direction: select an ink or adhesive lot and identify every affected finished package. Both directions matter for containment.
The Naike Group compliance documentation guide explains how project evidence is organized around market, product, material, and revision. Packaging inputs should sit in the same controlled project file rather than in an unrelated purchasing inbox.
Preserve the evidence after approval
A valid preproduction package can become unsupported when purchasing substitutes a material or the converter alters the process. Change control protects the reasoning that made the original evidence acceptable.
Require the supplier to notify changes before implementation and name the buyer role authorized to release them. Commercial urgency should trigger a documented risk decision, not silent substitution.
Use a Risk-Based Approval Gate Before Mass Production
Build the gate around unresolved questions, not the number of certificates collected. A low-complexity secondary carton with no plausible food transfer route may need a different evidence depth from a printed primary wrap around fatty food, but both need a documented rationale. Risk factors include directness of contact, food type, temperature, duration, print coverage, permeability, set-off opportunity, cure sensitivity, unknown composition, and market rules.
The packaging technologist should confirm construction and process, quality should confirm controls and traceability, procurement should confirm approved suppliers and change terms, regulatory staff should confirm the market basis, and the brand owner should approve the finished use and claims. Small teams can combine roles, but the questions still need named owners.
Close gaps explicitly. A missing migration assessment, unidentified adhesive, unverified cure window, incomplete supplier declaration, or report on the wrong structure is not made acceptable by a general factory certificate. Record the gap, risk, owner, due date, interim containment, and release decision.
Approval should reference exact files and revisions: dieline, artwork, bill of materials, declarations, assessment, test reports, process specification, inspection plan, golden sample, and deviation list. Signatures without referenced revisions can approve different documents in different departments.
For repeat orders, verify that the approved revision and materials are still active before releasing the purchase order. Compare the new bill of materials and artwork automatically where possible, then sample the evidence trail during incoming, production, and final inspection. A repeat SKU is not a reason to skip change review.
If the package or evidence cannot satisfy the destination requirement, keep the affected configuration unpublished, unproduced, or unreleased until the gap closes. Buyers can request a documented packaging compliance checkpoint with the intended market, food, structure, and supplier files attached.
Release one defined configuration
A gate should end with approve, approve with controlled limitations, or reject. Limitations belong on the production and sales record so the same package is not later used for a hotter fill, fattier food, longer shelf life, or different market without review.
Use the factory capability overview to align material, process, quality, and packaging discussions. Project-specific evidence still governs the final decision.
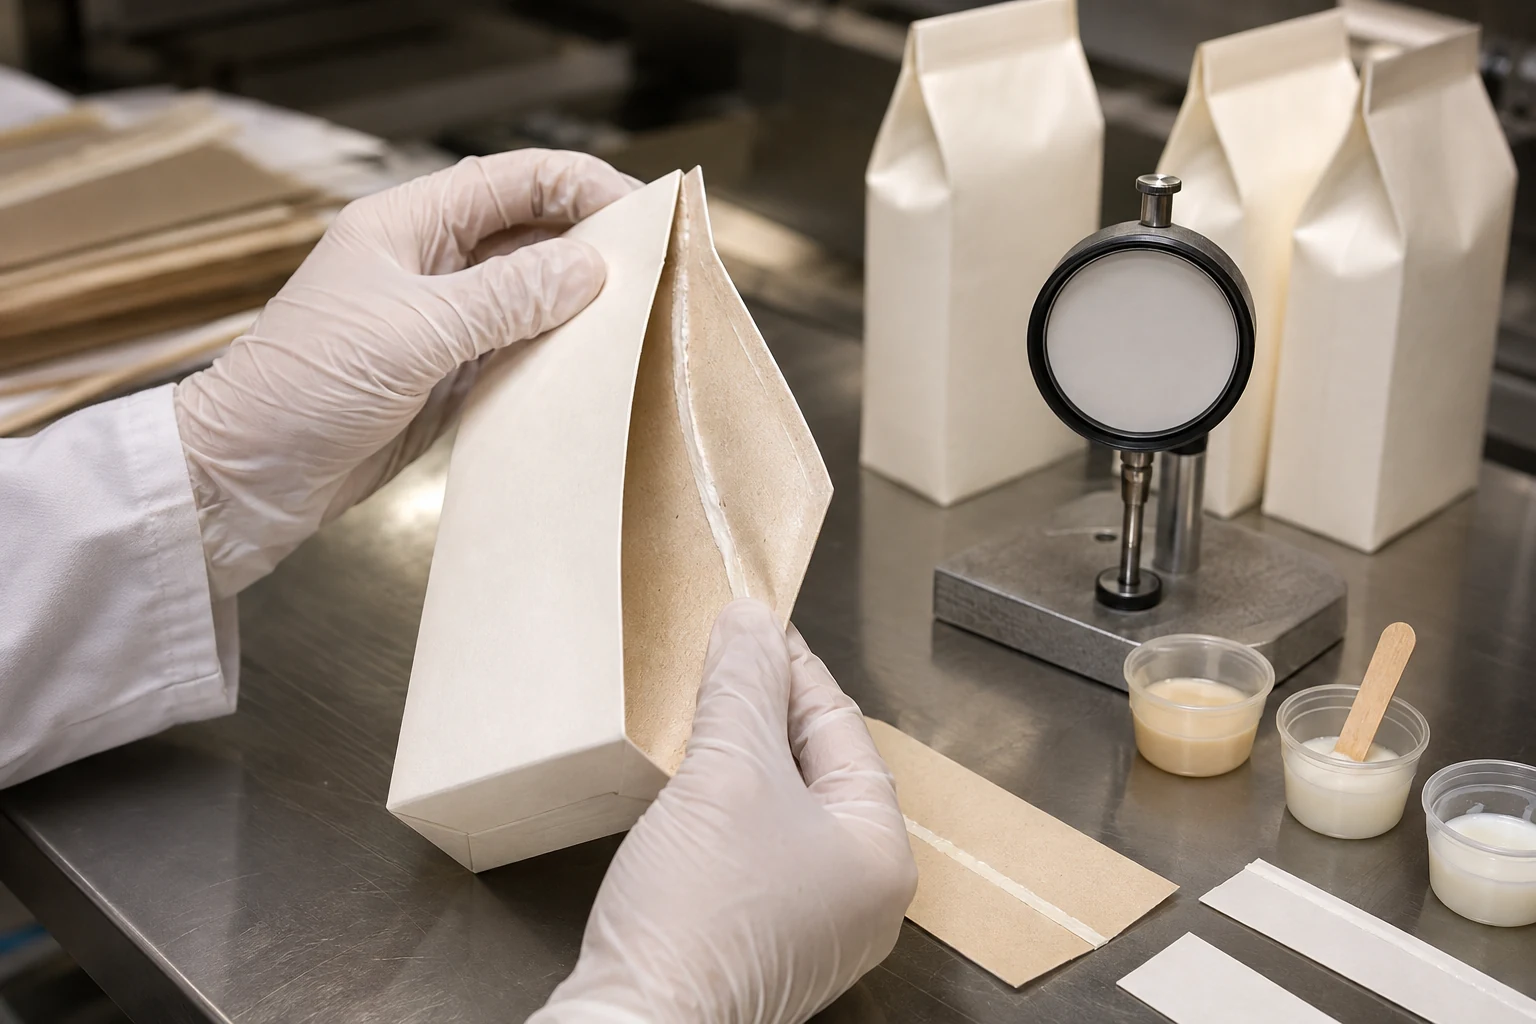
Food Packaging Ink Adhesive Compliance Requires Connected Proof
Treat the approved package as one evidence chain from intended use through raw materials, conversion, finished assessment, and shipment. A missing link should remain an open release item until a named owner supplies or resolves it.
Keep the chain concise enough for purchasing and production to use while retaining the technical files required for qualified review. Evidence quality is measured by relevance and traceability, not by the size of the certificate folder.
Food packaging ink adhesive compliance needs revision control
Reference exact documents, samples, product codes, and lots in the approval decision. Reopen the relevant assessment whenever a material, process, package, food, or market condition changes.
This final control makes the evidence durable across repeat orders. It also gives the buyer a clear reason to stop release when the supporting facts no longer match the commercial package.
Food Packaging Ink and Adhesive Evidence Matrix
This matrix separates documents that are often treated as substitutes. Each record answers a different question, so buyers should connect them rather than searching for one certificate that claims to cover everything.
| Evidence record | Primary question answered | Buyer verification |
|---|---|---|
| Finished-pack specification | What exact structure and intended use are being assessed? | Revision, layers, sides, food, time, temperature, shelf life, market |
| Technical data sheet | How should the commercial product be processed? | Product code, application, mixing, drying or cure, limits, version |
| Safety data sheet | How is the supplied chemical handled safely? | Identity, hazards, storage, revision; never treat as food-contact approval |
| Supplier declaration | What regulatory basis, restrictions, and assumptions support use? | Legal references, intended application, exclusions, downstream duties |
| Composition or restricted-substance statement | Which relevant constituents or limits need assessment? | Scope, thresholds, confidentiality route, formulation revision |
| Migration or risk-assessment report | Why is transfer acceptable for the defined use? | Sample identity, conditions, methods, limits, assumptions, conclusion |
| Production batch record | Was the approved material applied within the validated process? | Lots, ratios, coat weight, cure, line checks, deviations |
| Traceability and change log | Can evidence follow the lot and survive revisions? | Two-way lot mapping, notification, review, reapproval decisions |
Eight-Point Buyer Evidence Acceptance Checklist
Complete all eight rows before the packaging approval gate. A “yes” should point to a controlled file or production record rather than an email assurance.
| Check | Question | Why It Matters |
|---|---|---|
| Construction | Does the specification identify every substrate, print, coating, adhesive, side, and layer? | Defines the article actually assessed. |
| Intended use | Are food type, contact route, time, temperature, shelf life, and market recorded? | Prevents evidence from being applied outside its assumptions. |
| Material identity | Are trade names, product codes, colors, components, suppliers, sites, lots, and revisions controlled? | Stops generic declarations and silent substitution. |
| Regulatory statements | Do supplier files state the applicable basis, restrictions, exclusions, and downstream obligations? | Shows what the supplier conclusion does and does not cover. |
| Transfer rationale | Does testing or assessment address migration, set-off, barriers, curing, and relevant NIAS? | Connects input chemistry to foreseeable exposure. |
| Process control | Are application, drying, curing, coat weight, mixing, inspection, and deviation limits measurable? | Keeps production within the evaluated window. |
| Traceability | Can one finished lot be traced to every material lot and can an input lot be traced forward? | Enables containment and investigation. |
| Change approval | Must material, supplier, process, artwork, construction, use, or market changes be reviewed before release? | Preserves validity after the first approval. |
What Current Authoritative Sources Actually Establish
These sources illustrate why buyers need market-specific conclusions and a finished-use evidence chain. They do not create a universal approval for a named ink, adhesive, package, or supplier.
The European Union’s official Regulation (EC) No 1935/2004 text covers materials and articles intended or reasonably expected to contact food or transfer constituents under normal or foreseeable use. It establishes the framework expectation that materials should not transfer constituents in quantities that endanger health, unacceptably change food composition, or deteriorate organoleptic characteristics, while also requiring traceability. For a buyer, the practical record is therefore the connection between the finished printed package, its use, the supporting assessment, and its production identity.
The U.S. Food and Drug Administration’s official Food Contact Substance Notification inventory entry FCN 125 illustrates that an effective notification identifies a particular substance, notifier or manufacturer, intended use, and limitations, and it references adhesive use consistent with 21 CFR 175.105. This shows why an inventory entry or regulation number must be matched to the actual supplier, substance, adhesive application, package, and conditions rather than copied as a broad “FDA approved” statement.
The Swiss Federal Food Safety and Veterinary Office’s official packaging and printing-ink guidance explains that printing-ink substances and B2B declarations are addressed under the Swiss framework and that migration assessment depends on the food-contact material and worst-case use. It also notes that testing the ink alone generally cannot substitute for assessment of the final printed material. Buyers supplying Switzerland should therefore obtain the current destination-specific requirements and a declaration and assessment tied to the printed construction.
Practical disclaimer: food-contact, printing-ink, adhesive, NIAS, declaration, migration, labeling, and traceability requirements vary by jurisdiction and can change. Confirm the current law, official guidance, contractual duties, laboratory scope, and retailer rules with qualified specialists for the actual finished package and intended use before production, import, sale, or compliance claims.
Build the Approval File in Seven Controlled Steps
Step one freezes the intended use and finished construction. Assign revisions to the dieline, layer sequence, artwork, bill of materials, food-contact pathway, food type, time, temperature, shelf life, market, and distribution conditions.
Step two creates the approved-material register. List each ink color, additive, primer, coating, varnish, adhesive component, cleaner with relevant carryover, supplier, site, product code, lot fields, document revisions, allowed applications, restrictions, and review date.
Step three maps requirements to evidence. For every material and foreseeable transfer route, name the regulation, guidance, customer requirement, supplier declaration, composition information, calculation, migration test, barrier rationale, process control, or unresolved gap that supports the decision.
Step four validates the production-intent process. Run the real substrate, coverage, print sequence, adhesive amount, mixing, drying or curing, storage, stacking, and conversion conditions, then retain samples and machine records.
Step five reviews the finished package. Check migration or risk-assessment conclusions where applicable, sensory concerns, set-off, blocking, residual solvent, cure indicators, bond integrity, print rub, seam placement, barcode, artwork, and traceability against defined acceptance criteria.
Step six conducts a two-way trace exercise. Retrieve all input lots and evidence from a finished pack lot, then identify every finished pack and shipment made with a selected ink or adhesive lot. Resolve missing or slow links before release.
Step seven signs a revision-specific approval and change plan. State limitations, deviations, notification duties, document expiry or review dates, retained-sample location, and every change that triggers reassessment or testing.
Food Packaging Ink and Adhesive Record FAQ
Is an SDS enough to prove an ink or adhesive is suitable for food packaging?
No. An SDS primarily addresses hazard communication and safe handling of the supplied chemical. Suitability needs an intended-use and regulatory statement plus finished-package transfer reasoning, production controls, and traceability appropriate to the market.
Does printing only on the outside eliminate migration concerns?
Not automatically. Transfer may occur through a substrate, through the gas phase, or by set-off when printed and food-facing surfaces touch during winding, stacking, storage, or conversion. The real structure and process need review.
Can one migration report cover every artwork color and adhesive change?
Only when a documented assessment shows the tested sample remains representative or worst case. Changes in pigment, coverage, formulation, coat weight, substrate, barrier, cure, food, or conditions can require a new rationale or test.
What should buyers do when a supplier will not disclose a formulation?
Use a confidential disclosure route to a qualified laboratory or compliance reviewer and request a detailed declaration of restrictions and downstream duties. Confidentiality does not justify an evidence gap or a generic “food grade” claim.
How often should ink and adhesive declarations be renewed?
Set a risk-based review date and also review whenever regulation, supplier, site, formulation, product code, process, construction, intended use, or market changes. Purchasing controls should block documents marked obsolete or superseded.
Make the Evidence Chain Stronger Than the Certificate Stack
Reliable food packaging ink adhesive compliance comes from traceable alignment. The finished construction and foreseeable use define the question; supplier declarations and composition information explain the inputs; migration or risk reasoning addresses transfer; process records show controlled manufacture; and lot and change records preserve the conclusion.
A large folder can still fail if the documents refer to different products, revisions, substrates, markets, or conditions. Procurement should test every important claim by asking which exact package, lot, use, limit, and controlled record supports it.
Release only the defined configuration that passed the gate. When a supplier, material, artwork, process, food, shelf life, or market changes, reopen the affected part of the evidence chain before the modified package reaches production.
Request an Ink and Adhesive Evidence Review
Share the package construction, food-contact pathway, intended market, time and temperature conditions, artwork, ink and adhesive product codes, supplier declarations, migration evidence, and production controls. Naike Group can help organize the manufacturing-side evidence gaps for a controlled packaging approval.
Request a Custom Quote
Share your product, quantity, target market and customization needs. Our factory team will reply with the next practical step.
Continue Your Sourcing Research
The six newest factory-side articles are updated automatically by publication date.
Wheat Straw vs Bagasse Tableware: Buyer Comparison
A B2B decision guide comparing reusable wheat-straw polypropylene composite tableware with molded bagasse fiber formats across use, evidence, operations and end of life.
Can Wheat Straw Tableware Be Recycled? Buyer Q&A
A practical buyer answer on whether reusable wheat-straw composite tableware can enter PP recycling streams, which evidence matters, and how to qualify market claims.
Global SKU vs Regional SKU: Tableware Decision Guide
A buyer decision framework for choosing one global tableware SKU or controlled regional variants across compliance, packaging, logistics, inventory and change control.
Australia Food Packaging Evidence: Buyer Guide
A practical evidence guide for Australian food-packaging buyers covering intended use, migration risk, supplier assurance, testing, hygiene, release and change control.
EU PPWR Tableware Packaging vs Conventional Packs
A buyer comparison of PPWR-ready and conventional tableware packaging across product protection, material choices, empty space, evidence, labeling and release timing.
Prop 65 Tableware Requirements: Buyer Q&A
A practical buyer Q&A for defining California Proposition 65 exposure scenarios, evidence, warning decisions, supplier records and release controls for tableware.