Mold Cavity Count Selection: A Buyer Decision Guide
Choose cavity count from validated demand, effective output, tool architecture, process balance, equipment compatibility, and risk—not from the lowest quoted unit price.
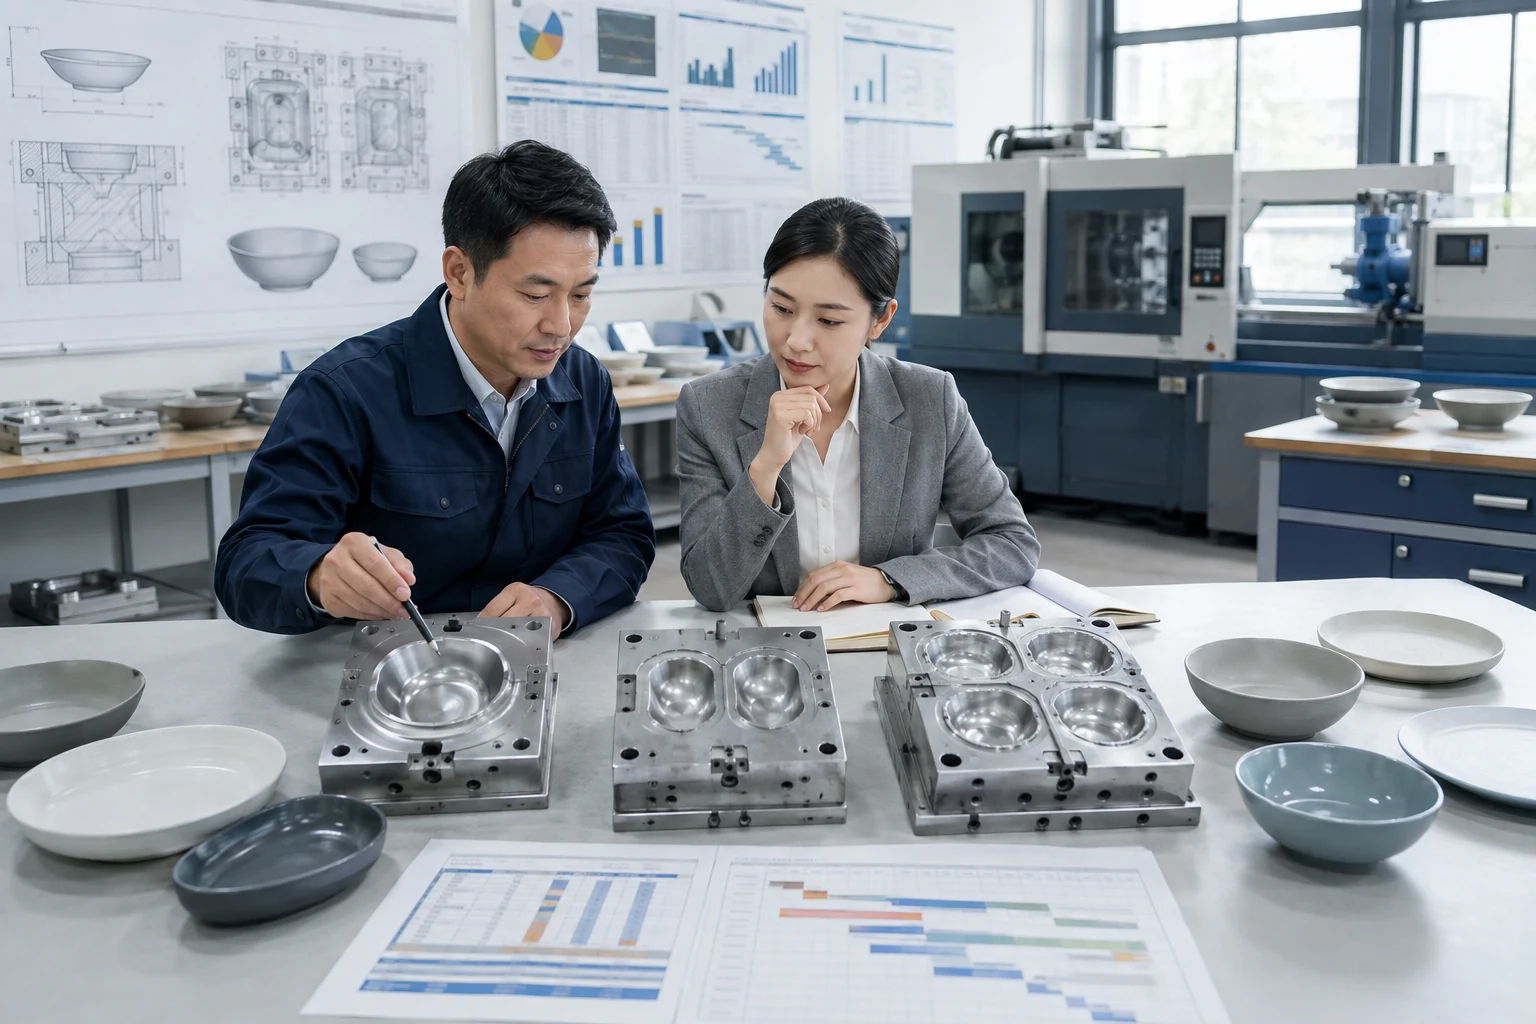
The right mold cavity count selection is the lowest-risk configuration that can deliver validated demand within available production time while meeting part quality, machine limits, maintenance needs, and investment targets. Buyers should compare effective accepted output, not simply multiply one cycle by the number of cavities, because balance losses, scrap, downtime, changeovers, and inspection can materially reduce real capacity.
A higher cavity count can lower molding cost per accepted part when demand is stable and the process is well balanced, but it raises tool size, complexity, capital exposure, repair scope, and dependence on one asset. A lower count can preserve flexibility and simplify validation, yet may require more machine hours or duplicate tools to protect supply.
This procurement guide applies the decision to molded custom tableware, including rigid plastics, wheat-straw composites, and silicone processes where tool architecture and cycle behavior differ. The final cavity decision must be confirmed by the mold designer and factory using the actual part, material, equipment, quality plan, and forecast.
Buyer Answer: Choose Cavities from Effective Demand Coverage
Model one, two, four, and any technically feasible higher-cavity option against peak monthly demand, required delivery window, accepted cycle time, planned shifts, realistic uptime, reject allowance, maintenance, sampling, and changeovers. Eliminate any option that exceeds machine shot, plasticizing, clamp, platen, utility, handling, or balance limits before comparing cost.
Then compare tool investment, unit conversion cost, cash exposure, spare strategy, expansion route, launch risk, and recovery if one cavity or the complete tool stops. Approve the cavity count only when the quotation states every assumption and the trial plan can verify cavity-to-cavity consistency.
Translate the Sales Forecast into Accepted Parts per Hour
Start with a dated demand model rather than an annual volume headline. Break demand into launch, normal, promotion, seasonal peak, safety-stock recovery, and growth scenarios, then state the delivery window for each. A million units across twelve steady months creates a different tooling decision from the same volume concentrated in one retail season.
Calculate the required accepted output at the factory gate. Include the pieces per retail set, color mix, packaging assortment, buyer inspection allowance, and the fact that rejected or reworked pieces do not satisfy demand. If one order requires four plates, two bowls, and four cups, each product family needs its own capacity model rather than one blended number.
Available production time must reflect the real calendar. Remove planned maintenance, mold cleaning, material and color changes, trial runs, holidays, engineering access, and capacity already committed to other programs. A theoretical twenty-four-hour schedule is not a credible quotation unless the factory has documented staffing, utilities, material flow, and maintenance coverage for it.
Use demonstrated or conservatively estimated cycle time for the actual geometry and material. Cooling can dominate rigid tableware cycles, while cure, loading, demolding, and secondary handling may dominate silicone or compression routes. A supplier should show which portion of cycle time is simulated, based on a comparable tool, or demonstrated on production-intent equipment.
Apply realistic uptime and yield separately. Four cavities running at ninety percent uptime and ninety-five percent first-pass yield produce fewer accepted parts than the simple cavity-times-cycles calculation suggests. Keep both factors visible so a low yield is not disguised as maintenance downtime or recovered by optimistic overtime.
Buyers can send the demand curve and target delivery window for a cavity-capacity review. The useful output is a scenario table showing required hours, available hours, reserve, and the exact assumption that changes the recommended cavity count.
A mold cavity count selection formula is only a screening tool
A screening equation can divide required good parts by cycles available, uptime, and yield to estimate cavities. It cannot decide whether the proposed runner, cooling, ejection, mold base, or machine can make those cavities behave consistently.
Round-up logic also needs commercial judgment. If the result is slightly above two cavities, the right answer might be a four-cavity tool, two duplicate single-cavity tools, a longer schedule, or a design and cycle improvement; the equation does not choose among those risk profiles.
Check Machine, Material, Part, and Tooling Constraints
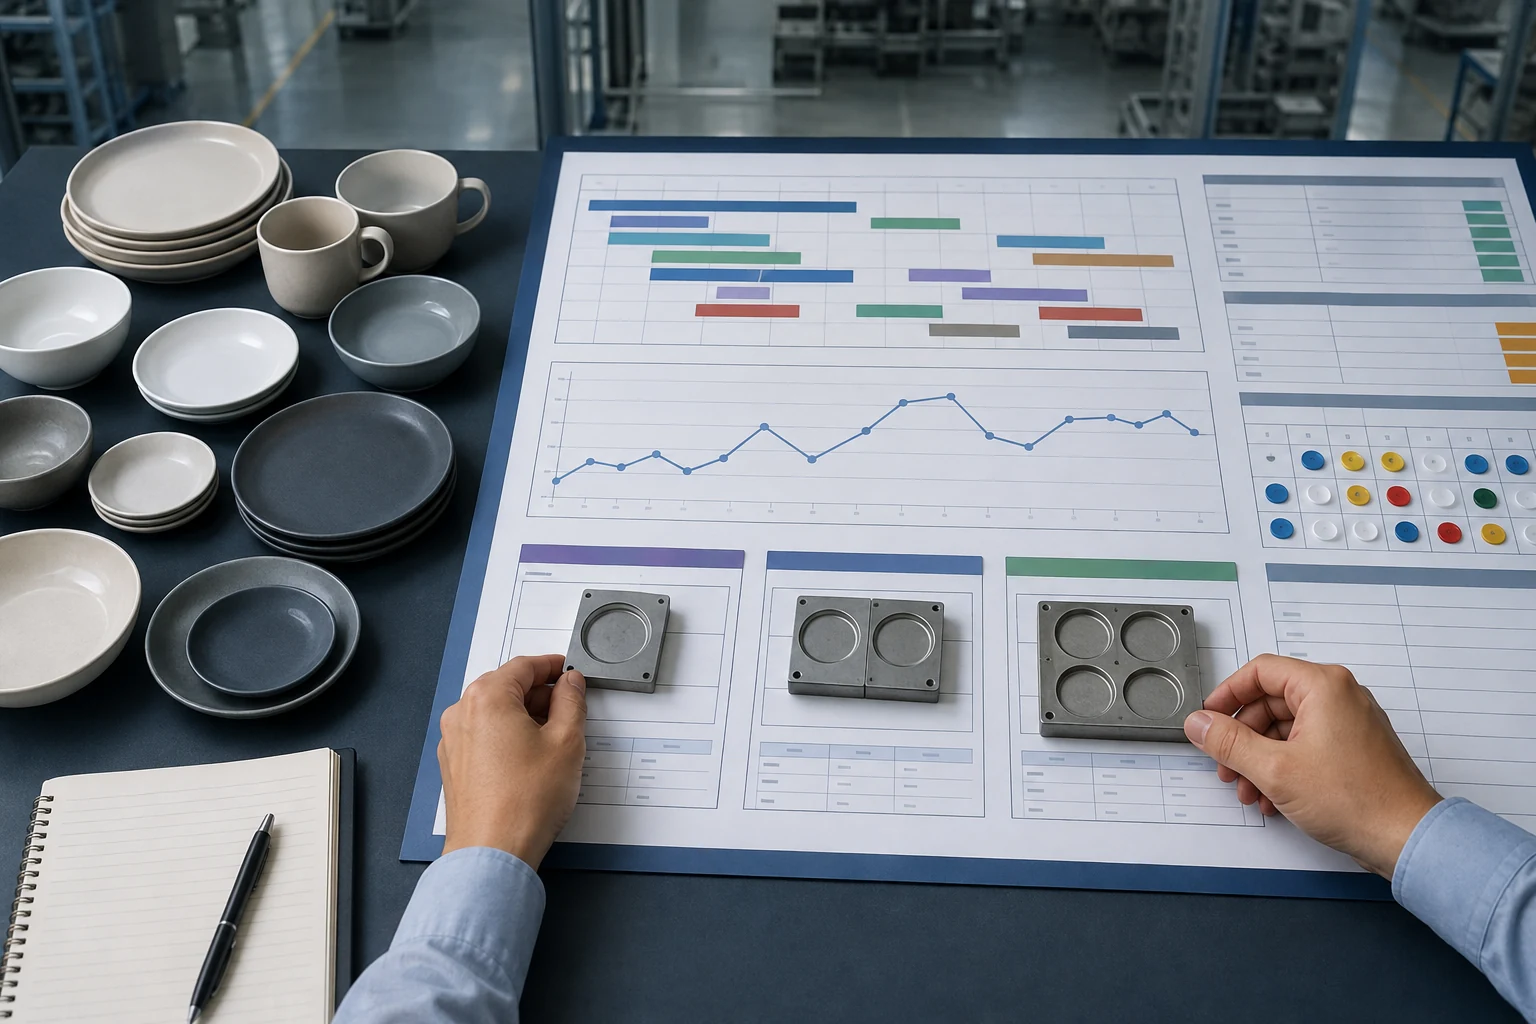
The proposed mold must fit the intended press or molding system. Review platen dimensions, tie-bar spacing, mold thickness range, opening stroke, daylight, ejection, clamp force, shot capacity, plasticizing capacity, injection pressure, nozzle interface, utilities, lifting, and robot or manual part removal. A cavity count that forces the project onto scarce equipment can erase the apparent capacity advantage.
Shot-size checks should include the combined part and runner mass and preserve a suitable operating range for the actual machine. Plasticizing capacity must replenish material within the cycle without degrading it, while clamp calculations consider projected area and cavity pressure. Buyers should ask the factory to identify the named machine class and the limiting calculation rather than state only that the tool “fits.”
Part geometry affects how efficiently cavities can be arranged. Large plates and divided trays consume projected area and mold-base space, while deep cups can require longer opening stroke and more complex ejection. Slides, lifters, inserts, unscrewing features, or delicate textures may reduce practical cavity count even when material volume appears small.
Material behavior changes the feasible architecture. Flow length, viscosity, fiber or filler content, shrinkage, cure behavior, venting, temperature sensitivity, and allowable residence time affect runner size and balance. Wheat-straw composite formulations can require particular attention to flow and appearance, while silicone tooling may depend on metering, cold-runner, vacuum, and demolding choices.
Cooling or heating capacity must be uniform across the tool. Packing more cavities into a mold base can create circuit congestion, temperature differences, longer cycles, and uneven shrinkage. The quotation should state whether cycle estimates include production-intent thermal design, manifolds, controllers, and utility conditions.
Handling also sets a practical limit. Parts must be ejected or removed without distortion, scratches, mixing, or unsafe manual reach, then identified and transferred to trimming, decoration, assembly, or inspection. Automation cost and floor space belong in the cavity decision when downstream operations cannot absorb the nominal molding output.
The factory should disclose the binding constraint
One option may be limited by clamp force, another by shot volume, and another by balance or cooling. Requiring the supplier to name the binding constraint makes quotations comparable and gives engineering a clear target for verification.
The custom mold and tooling pathway provides context for tool development, but machine compatibility and cavity feasibility remain specific to the approved product and factory configuration. Confirm both before the tool design is released.
Test Whether Every Cavity Can Make the Same Approved Part
Multi-cavity tooling must fill, pack, cool or cure, and eject parts consistently. Runner length, diameter, gate position, pressure loss, temperature, venting, and cavity geometry influence balance. If one cavity fills early while another fills late, the process window may force a choice between flash, short shots, dimensional drift, or appearance differences.
Naturally balanced runner layouts can simplify equal flow paths, although mold size and part geometry may make them difficult. Artificial balancing, hot runners, valve gates, or process adjustments can help, but they add design decisions, controls, maintenance, and validation needs. Buyers should request the proposed feed-system concept before treating every cavity count as equivalent.
Cavity-to-cavity cooling deserves equal attention. Different circuit lengths, flow rates, hot spots, or insert contact can create uneven cycle readiness and shrinkage. A tool may produce the required quantity while one cavity still creates more warpage, gloss variation, sticking, or dimensional loss than the others.
The first-article and trial plan should identify samples by cavity. Record part weight, critical dimensions, appearance, function, and defect data for consecutive cycles after stable conditions are reached. Pooled averages are weak evidence because a strong cavity can conceal a marginal one.
Define what happens when one cavity fails. The tool may allow a cavity to be safely blocked, but output, runner balance, pressure, cycle, and quality can change. The buyer needs an approved reduced-cavity process and revised capacity plan instead of assuming production continues normally.
Do not accept “four cavities means four identical parts” as the validation conclusion. Require design review, analysis where justified, mold trial evidence, cavity-level approval, and a control plan that preserves cavity identity when risk warrants it.
Balance evidence belongs in the purchase decision
A higher-cavity quote should identify how the feed system, temperature control, venting, ejection, and process window support equal results. If the supplier cannot explain the validation method, the quoted unit saving remains speculative.
Cavity-level evidence also shortens correction. Quality and tooling teams can distinguish a local insert or cooling issue from a machine, material, or whole-tool problem before approving expensive changes.
Compare Total Program Economics, Not Tool Price Alone
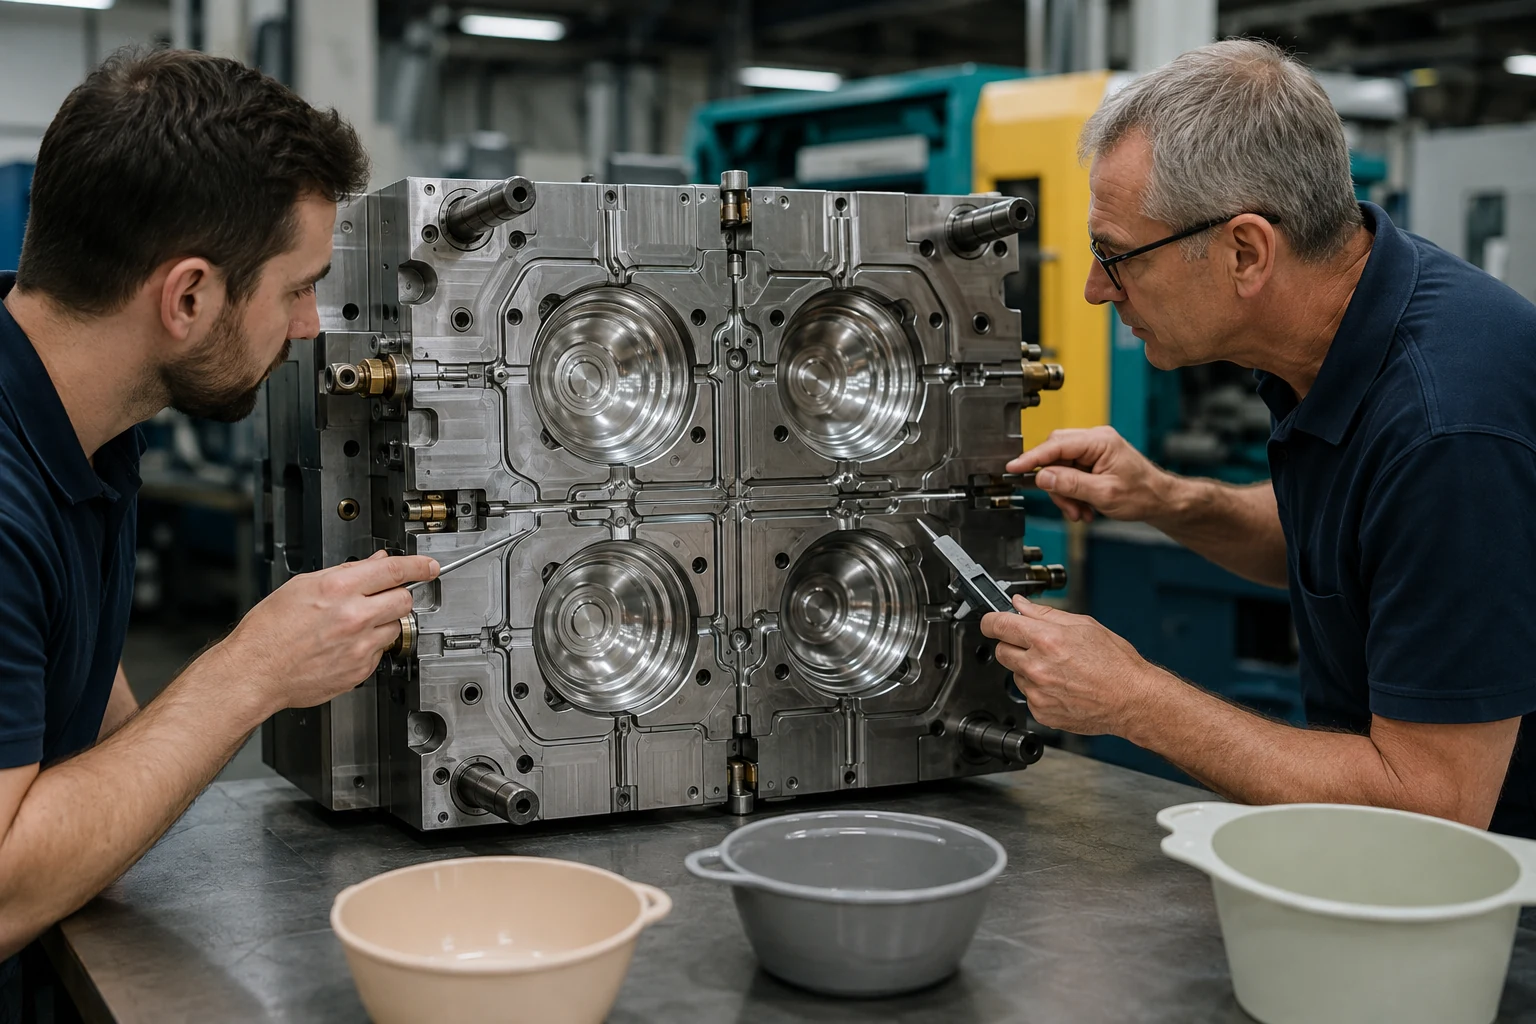
The economic comparison should separate one-time and recurring costs. One-time items include mold design, steel or aluminum, inserts, hot-runner or cold-runner systems, controllers, simulation, fixtures, trials, gauges, spares, validation, and engineering changes. Recurring items include machine time, labor, material and runner waste, energy, maintenance, quality checks, scrap, packaging flow, and depreciation assumptions.
A higher cavity count commonly increases upfront investment while reducing machine cycles per accepted part. The crossover point depends on actual demand and realized yield, not the supplier’s maximum forecast. Model at least a conservative, expected, and upside volume so procurement can see when the additional cavities earn back their cost and when they become stranded capacity.
Cash timing matters. A four-cavity tool may require more capital before the buyer has validated market demand, while a smaller tool can preserve launch flexibility. Conversely, underbuilding capacity may force overtime, premium freight, lost sales, or an urgent second tool whose timing and product match are harder to control.
Runner and material economics should be explicit. Cold-runner systems can add scrap or regrind handling, while hot-runner systems can reduce runner waste but add purchase, control, maintenance, color-change, and downtime considerations. The right comparison uses material value, quality restrictions, color frequency, and maintenance capability for the actual program.
Tool life and maintenance cost should be tied to the planned number of cycles and product risk. More cavities mean more gates, vents, inserts, ejectors, seals, and surfaces to maintain, although total cycles for a given volume may fall. Ask for preventive-maintenance intervals, expected wear components, spare strategy, repair access, and the output impact of planned service.
Include downstream capacity in the unit-cost model. Molding eight pieces per cycle is not valuable if trimming, decoration, assembly, inspection, or packing can accept only four. Bottleneck movement can increase work in process, handling damage, mixed cavities, and labor instead of lowering landed cost.
Calculate the cost per accepted and delivered piece
Quoted molding price should be reconciled with yield, inspection, packaging, and logistics assumptions. A lower price per molded shot may not produce a lower cost per accepted retail-ready unit.
Require the supplier to show the same demand, uptime, yield, cycle, material, labor, and amortization basis for every cavity option. Comparable assumptions expose whether the saving comes from engineering or from moving risk outside the quote.
Choose Between One Large Tool and Multiple Smaller Tools
One high-cavity tool concentrates output and technical knowledge in a single asset. It can simplify scheduling and reduce duplicate setup, yet a major mold or machine failure may stop the entire stream. Multiple smaller tools can provide redundancy, phased investment, geographic flexibility, or parallel colors, but they require matched approvals and can increase total tooling and maintenance work.
Duplicate tools are not automatically identical. Steel, machining, polishing, texture, gate finish, cooling, sensors, and process equipment can create differences even from the same drawing. Buyers planning parallel production should define a common product standard, tool identification, golden samples, cavity mapping, validation, and change control across every tool.
Color and product mix can favor smaller independent tools. A single four-cavity mold running one color changes all four outputs together, while two tools may support separate colors or order priorities. Family tools that produce different components in one cycle can help set ratios, but demand imbalance, differing fill behavior, or rejected components can create waste.
Geographic or supplier redundancy adds commercial questions. Tool ownership, transfer rights, duplicate data, spare inserts, confidentiality, customs, and receiving-factory compatibility should be agreed before risk materializes. A second tool that cannot be accessed or qualified quickly is not effective contingency capacity.
The recovery plan should model partial and total loss. Ask how production changes when one cavity is blocked, an insert is damaged, a controller fails, the named press is unavailable, or the whole tool needs off-site repair. State the inventory buffer and maximum acceptable recovery time for each scenario.
For early demand, a staged route can be sensible. Launch with a lower-cavity production-intent tool or approved bridge option, confirm demand and process evidence, then add an insert, companion tool, or higher-cavity platform if the design allows. The expansion route must be engineered before assuming that cavities can simply be added later.
Resilience has a measurable commercial value
Compare not only average cost but also lost-output exposure and recovery time. Procurement can assign scenario probabilities or use a qualitative risk score when reliable probabilities do not exist.
A resilient option may cost more per nominal piece while protecting a critical retail launch or replenishment program. That premium should be visible and deliberate rather than buried in a general preference for more tooling.
Write the Cavity Decision into the RFQ, Trial, and Purchase Order
The RFQ should request at least two technically feasible cavity scenarios when uncertainty is material. For each option, ask for tool architecture, mold size and weight, intended machine class, runner system, cycle basis, nominal and accepted hourly output, yield, uptime, maintenance, trial plan, lead time, investment, unit cost, and exclusions.
Require the supplier to identify assumptions that still need validation. These can include final material, wall thickness, shrinkage, gate location, surface finish, automation, cycle time, cooling, cavity balance, packaging flow, and annual volume. An assumption register prevents a provisional quote from being treated as a fixed manufacturing promise.
The design-review gate should confirm the cavity layout and major interfaces before steel is cut. Review feed and thermal concepts, parting, ejection, cavity identification, interchangeability, wear components, sensors, lifting, utility connections, and safe maintenance access. Record approved changes and their effect on output and cost.
The trial protocol should define stable-start criteria, consecutive cycles, samples per cavity, dimensions, weight, appearance, functional checks, defects, process settings, cycle components, and the disposition of any rework or blocked cavity. Production release should depend on accepted evidence rather than tool completion or sample shipment alone.
The purchase order must describe ownership, custody, permitted use, preventive maintenance, repairs, spare parts, data deliverables, change approval, storage, insurance, transfer conditions, and end-of-program disposition. Cavity count is an asset decision, so the commercial terms must protect the buyer’s ability to maintain and recover that capacity.
If your team needs a structured comparison, request a tooling quotation review before authorizing the mold. Share the forecast scenarios, product revision, material, target cycle, delivery window, quality plan, equipment constraints, and required contingency route.
The approval memo should explain why this cavity count wins
Record the rejected alternatives and their decisive constraints, not just the chosen number. Future teams can then revisit the decision when demand, product design, equipment, or supply risk changes.
A concise approval memo should link the selected option to capacity calculations, technical review, economics, trial criteria, and contingency. That record is more durable than a purchasing note that approves four cavities without explaining the basis. Keep the signed rationale with the tooling file.
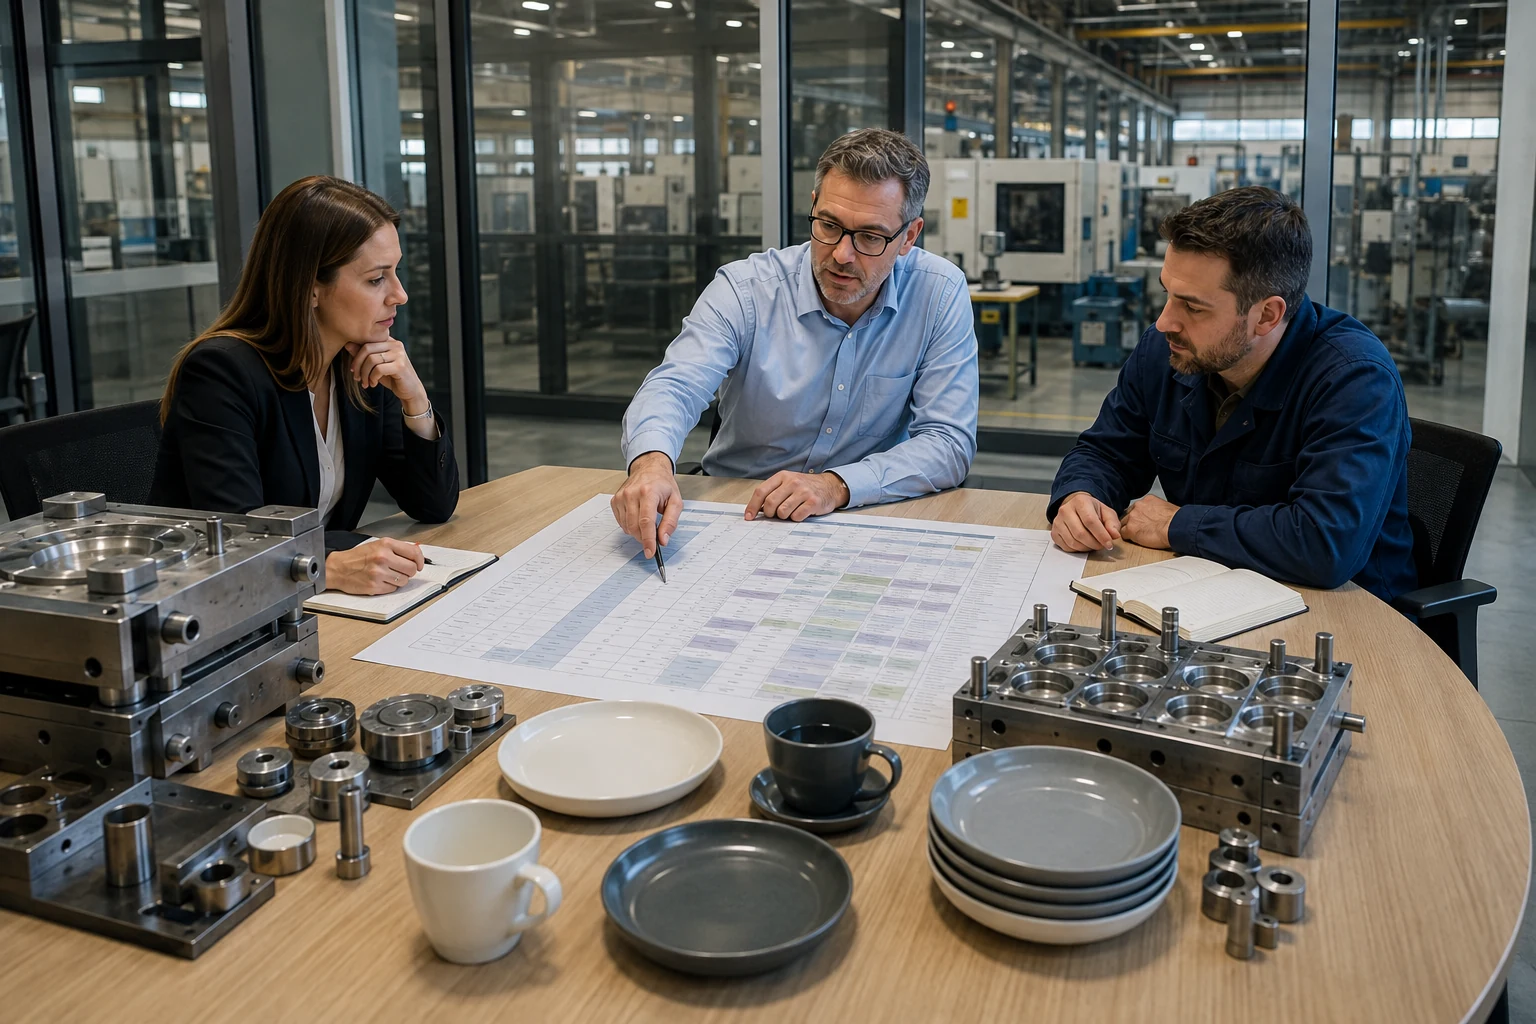
Cavity Strategy Comparison for Custom Tableware
No cavity count is universally best. Use this comparison to shortlist the configuration whose capacity, capital, flexibility, and recovery profile match the buyer’s actual demand and risk.
| Decision criterion | Single cavity | Two cavities | Four or more cavities |
|---|---|---|---|
| Best-fit demand | Launch, low volume, uncertain forecast | Moderate repeat demand or staged growth | Stable high volume with tight delivery windows |
| Upfront investment | Usually lowest tool complexity | Higher tool and validation investment | Highest tool, feed, thermal, and automation exposure |
| Nominal output | Lowest per cycle | Higher with manageable multiplication | Highest only when every cavity and downstream step performs |
| Balance and validation | Simplest cavity evidence | Requires cavity-to-cavity comparison | Requires robust balance, thermal, ejection, and cavity controls |
| Machine flexibility | Often broader equipment choice | May narrow compatible press range | Can depend on larger or scarcer dedicated equipment |
| Product or color flexibility | Simple changeover but one stream | Can split across two tools only if separately built | One large tool usually commits all cavities to one setup |
| Failure exposure | One cavity stops the tool | One blocked cavity may reduce output | A whole-tool failure stops substantial capacity |
| Expansion route | Duplicate or replace tool later | Add a matched tool or new platform | Expansion may require another large capital step |
B2B Buyer Mold Cavity Decision Checklist
Complete this checklist before approving tool design. Each answer should point to a calculation, drawing, quotation line, trial method, or named responsibility.
| Check | Question | Why It Matters |
|---|---|---|
| Demand | Are launch, expected, peak, and downside volumes dated and separated? | Prevents the annual forecast from hiding seasonal overload or stranded capacity. |
| Output | Does capacity use accepted parts, realistic cycle, uptime, yield, and available hours? | Replaces nominal cavity multiplication with deliverable output. |
| Equipment | Does the named machine satisfy shot, plasticizing, clamp, platen, stroke, utility, and handling needs? | Avoids dependence on an incompatible or unavailable press. |
| Balance | Does the design explain runner, gate, temperature, venting, cooling or cure, and ejection balance? | Protects cavity-to-cavity quality and cycle stability. |
| Economics | Are tool, unit, material, maintenance, validation, automation, and downstream costs compared? | Shows the true program crossover instead of tool price alone. |
| Resilience | What happens if one cavity, the press, or the whole mold is unavailable? | Quantifies output loss, buffer, and recovery time. |
| Evidence | Will trials identify consecutive samples and results by cavity? | Stops averages from concealing a marginal cavity. |
| Control | Are ownership, changes, repairs, spares, data, transfer, and reinspection terms written? | Protects the purchased capacity throughout the program. |
Technical Sources That Frame the Cavity Decision
These technical references support the engineering logic behind a buyer’s decision, but they do not validate a particular Naike Group quotation or replace analysis and trials for the actual product, material, mold, and machine. Apply them to the controlled project inputs.
Autodesk’s guidance on selecting the number of cavities identifies production schedule, required quantity, part shape and size, mold cost, machine clamp force, shot volume, and plasticizing capacity as relevant constraints. The procurement implication is to calculate several limits and use the binding result rather than choose a cavity number from demand alone.
Autodesk’s multi-cavity flow-balance guidance explains that cavities should fill simultaneously and that unequal flow paths can produce short shots, overpacking, or flash. This supports requiring a documented runner concept and cavity-level trial evidence before treating theoretical output as approved capacity.
Autodesk’s runner-layout guidance notes that runner design affects material usage and part quality and calls for cavity count, material, processing conditions, and flow balance to be considered together. Buyers should therefore evaluate cavity count as part of a complete tooling and process proposal rather than as an isolated commercial option.
Practical disclaimer: this article is procurement and manufacturing guidance, not a mold-design approval, capacity guarantee, financial forecast, or substitute for qualified engineering review. Confirm calculations, material behavior, machine limits, tool architecture, safety, validation, intellectual property, and commercial terms for the actual project before committing capital.
A Seven-Gate Decision Path Before Tool Authorization
Gate one fixes the demand envelope. Procurement and sales approve launch, expected, peak, downside, promotion, and replenishment scenarios with dated delivery windows, set quantities, color mix, and service buffer. Unknown demand remains an explicit scenario rather than an inflated forecast.
Gate two calculates effective output. The factory documents cycle basis, cavity count, yield, uptime, shifts, available hours, maintenance, changeovers, and downstream constraints for each option. The buyer checks accepted parts against every demand scenario and records the remaining capacity reserve.
Gate three closes equipment limits. Tooling and process engineers identify the intended machine class and verify clamp, shot, plasticizing, platen, stroke, ejection, injection pressure, utilities, controls, lifting, and handling. Any dependency on one scarce press appears in the risk register.
Gate four reviews mold and flow architecture. The team examines cavity layout, feed balance, gate strategy, thermal circuits, venting, ejection, cavity identification, wear components, service access, and the effect of blocking a cavity. Analysis or comparable production evidence supports assumptions where risk warrants it.
Gate five compares total economics. Finance and procurement model tool and validation investment, unit conversion, material and runner treatment, labor, energy, maintenance, spares, automation, inspection, scrap, packaging flow, and possible expansion. The approval states the volume and time horizon at which the preferred option becomes favorable.
Gate six tests resilience. The buyer compares one large tool, multiple tools, staged investment, inventory buffer, spare inserts, and recovery routes for partial or complete downtime. Ownership, custody, transfer, repair, and duplicate-tool controls are settled before they become urgent.
Gate seven defines proof and release. The purchase order links payment and production authorization to design review, stable trials, cavity-level samples, actual results, cycle evidence, corrections, and signed approval. Changes after release trigger a documented assessment and the required partial or full revalidation.
The final memo should state why the selected cavity count wins under the approved assumptions and which event would reopen the decision. A large forecast change, product redesign, material change, new machine, packaging bottleneck, or altered risk tolerance can justify a new comparison.
Mold Cavity Count Selection FAQ for B2B Buyers
Does doubling mold cavities always double production output?
No. Real output also depends on cycle time, uptime, yield, runner and thermal balance, handling, secondary operations, inspection, and available machine hours. Buyers should compare accepted parts per hour and delivery coverage.
Is a four-cavity mold always cheaper per part than a two-cavity mold?
It can reduce machine cycles per piece at sufficient stable volume, but higher tooling, validation, maintenance, automation, scrap, and downtime exposure may delay or eliminate the saving. Model total program cost across realistic demand scenarios.
Can one failed cavity be shut off while the others keep running?
Sometimes, if the tool and process are designed for safe cavity blocking and the revised flow, pressure, cycle, and quality remain validated. The factory should define the reduced-output route before relying on it as contingency.
Should different tableware pieces share one family mold?
A family tool can produce matched components per cycle, but different volumes, flow behavior, cooling, rejection rates, or demand ratios can create imbalance and waste. Compare it with independent tools using the actual set mix and quality risks.
When should a buyer approve a second tool instead of more cavities?
A second tool may be preferable when the program values redundancy, separate colors, phased investment, geographic flexibility, or access to different machines. It also requires matched validation, standards, maintenance, and change control.
Approve the Capacity System, Not the Largest Cavity Number
A defensible mold cavity count selection connects dated demand with accepted output, machine and material constraints, cavity balance, total economics, downstream capacity, validation evidence, and recovery planning. The chosen number is an output-and-risk system, not a badge of tooling sophistication.
Buyers should reject both automatic minimalism and automatic multiplication. One cavity may constrain growth, while many cavities may lock capital into a complex asset whose real process window and demand case are unproven.
Authorize the configuration whose assumptions can be tested and whose failure modes have affordable responses. That decision gives procurement a clearer cost basis, gives tooling teams a measurable target, and gives operations a capacity plan they can actually deliver.
Request a Mold Capacity Decision Review
Share the product drawing, material, forecast scenarios, delivery windows, intended equipment, target cycle, quality requirements, packaging flow, and contingency expectations. Our manufacturing team can compare feasible cavity routes before tool authorization.
Request a Custom Quote
Share your product, quantity, target market and customization needs. Our factory team will reply with the next practical step.
Continue Your Sourcing Research
The six newest factory-side articles are updated automatically by publication date.
Wheat Straw vs Bagasse Tableware: Buyer Comparison
A B2B decision guide comparing reusable wheat-straw polypropylene composite tableware with molded bagasse fiber formats across use, evidence, operations and end of life.
Can Wheat Straw Tableware Be Recycled? Buyer Q&A
A practical buyer answer on whether reusable wheat-straw composite tableware can enter PP recycling streams, which evidence matters, and how to qualify market claims.
Global SKU vs Regional SKU: Tableware Decision Guide
A buyer decision framework for choosing one global tableware SKU or controlled regional variants across compliance, packaging, logistics, inventory and change control.
Australia Food Packaging Evidence: Buyer Guide
A practical evidence guide for Australian food-packaging buyers covering intended use, migration risk, supplier assurance, testing, hygiene, release and change control.
EU PPWR Tableware Packaging vs Conventional Packs
A buyer comparison of PPWR-ready and conventional tableware packaging across product protection, material choices, empty space, evidence, labeling and release timing.
Prop 65 Tableware Requirements: Buyer Q&A
A practical buyer Q&A for defining California Proposition 65 exposure scenarios, evidence, warning decisions, supplier records and release controls for tableware.