Silicone Tableware Color Tolerance: Buyer Approval Guide
A practical framework for importers and private-label teams that need commercially consistent silicone colors across components, production lots and repeat orders.
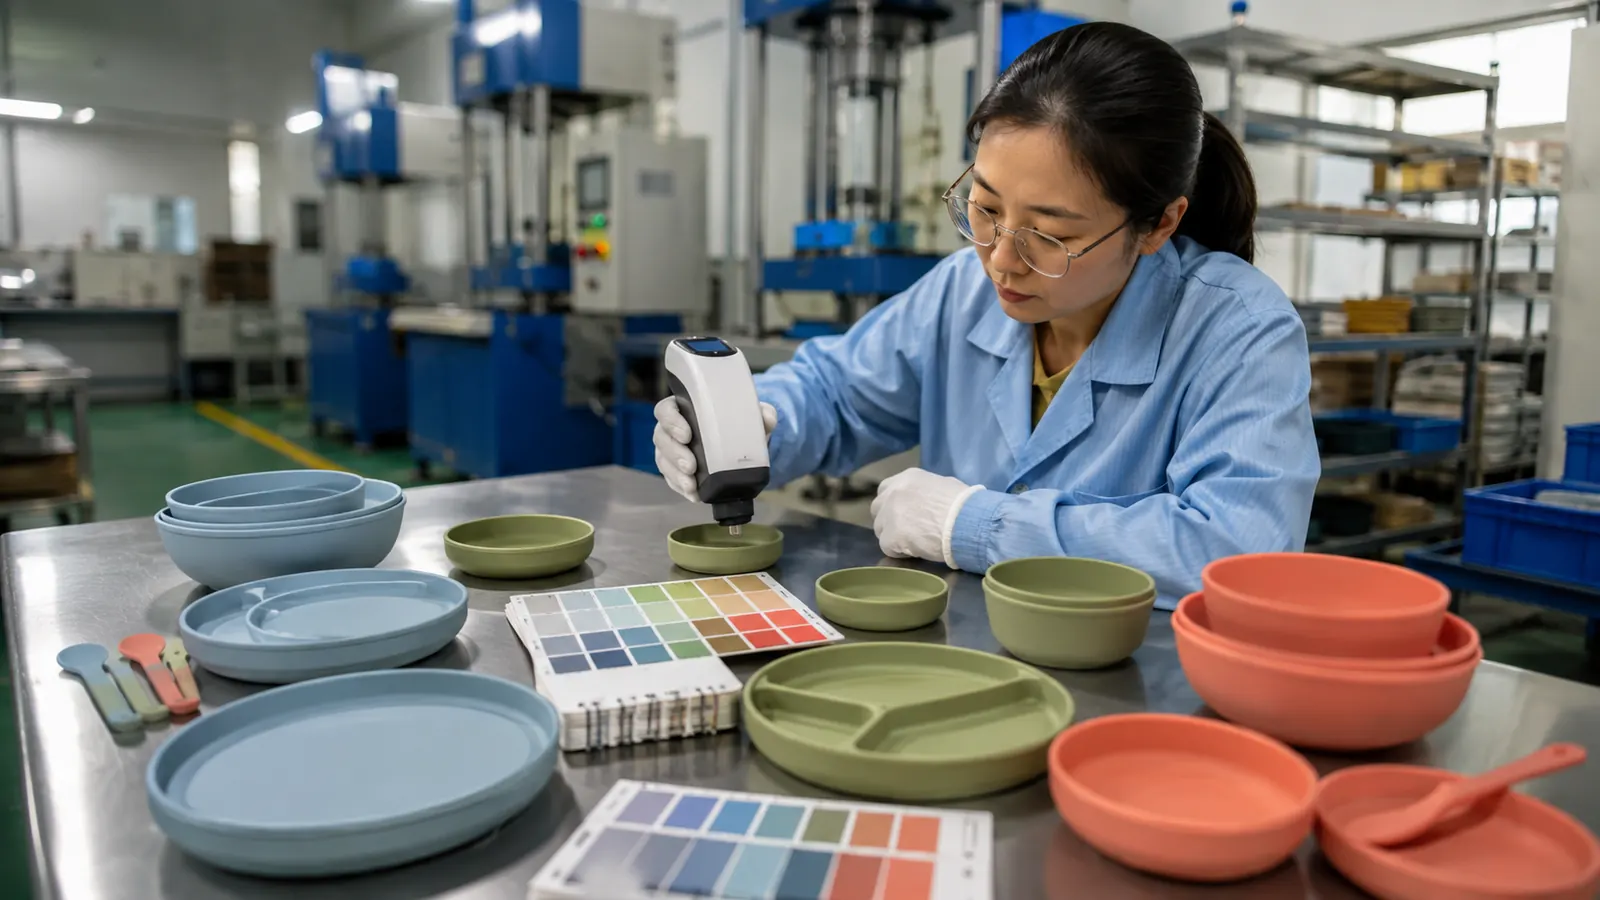
Silicone tableware color tolerance is the agreed boundary between acceptable production variation and a color difference that requires correction or buyer review. It should be established on the actual silicone formulation, molded surface and product geometry rather than copied from a paper swatch or an unrelated plastic part.
Naike Group manufacturing team treats color as a controlled approval path within our OEM/ODM customization workflow. Buyer references, formulation trials, physical samples, measurement settings and bulk-production records must point to the same released standard.
This guide helps sourcing, product and quality teams decide what evidence to request before quotation and shipment. For a project-specific review, send our factory your product files, target colors and market requirements before finalizing the sample plan.
Factory insider takeaway: Do not approve a color name alone. Approve a material construction, physical reference, viewing method, measurement setup, tolerance, sampling rule and change-control trigger that can be repeated during bulk production.
What Silicone Tableware Color Tolerance Actually Controls
A tolerance does not promise that every point on every molded component will produce an identical reading. It defines how far production may move from an approved target before the difference becomes commercially or technically unacceptable.
The visible result is influenced by pigment concentration, silicone base, opacity, wall thickness, texture, gloss, cure history and the light used for inspection. A flat plaque and a deep suction bowl may therefore appear different even when both use material prepared from the same approved color direction.
Buyers should separate hue or lightness drift from surface defects. Flow marks, contamination, uneven gloss and local scorching require their own acceptance language because an average color number can hide a visible defect.
A workable specification identifies whether control applies to each component independently or to the assembled retail set. Set-level coordination matters when a plate, bowl, bib and cup will be photographed or displayed together.
Why silicone tableware color tolerance must be product specific
Generic numerical limits may be too loose for a premium pastel collection or unnecessarily tight for a promotional item. The factory and buyer should evaluate actual trial parts under the intended viewing conditions before fixing the final boundary.
The approved limit must also be achievable through the selected formulation and process. An unrealistic number increases sorting, delays and disputes without guaranteeing a better consumer impression.
Build the Approval Standard before Requesting Bulk Color
Begin with a complete brief that names the product revision, silicone construction, surface finish, component list, target market and color reference. Color work performed before those decisions are stable may need to be repeated after a geometry, material or texture change.
A Pantone reference can communicate direction, but printed paper and molded silicone reflect light differently. The factory should translate the reference into a production-intent sample rather than claiming that a code alone guarantees a visual match.
Physical references should be labeled with color code, material, part revision, approval status and date. Unidentified samples can be confused with development trials or rejected versions and should never govern a repeat order.
When several components form one kit, approve the complete arrangement. Differences that seem minor when parts are viewed separately may become obvious when matching products sit beside each other in retail packaging.
Which reference should govern when files disagree
The project record should state whether the signed physical sample, measured dataset or another approved master has priority. Digital renderings and phone photographs are useful communication aids but are not stable color standards.
Our silicone Pantone color matching guide explains how a design reference becomes a controlled molded result. Use that process before attaching a fixed color promise to the purchase order.
Evaluate Silicone Colors under Relevant Lighting
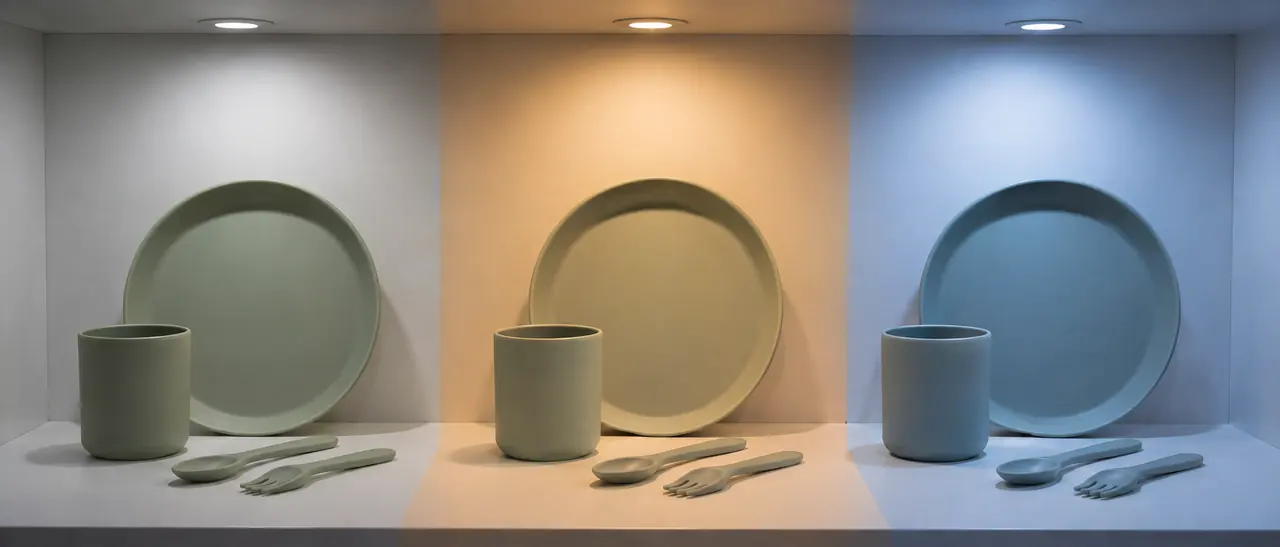
A sample may match under daylight and separate under warm retail or cool warehouse lighting. This effect becomes important when different pigment systems or materials are compared across a coordinated collection.
Select viewing conditions that represent the buying decision and the sales environment. A general daylight condition supports routine comparison, while a retailer may add store lighting and an e-commerce team may add the controlled light used for product photography.
Keep the booth background, lamp condition, sample orientation and observer adaptation consistent. Curved surfaces should be viewed from agreed angles because reflections can make one area look lighter or glossier than another.
Record whether a concern occurs under all specified lights or only one. That evidence helps the buyer decide whether reformulation is justified instead of repeatedly changing color from subjective messages.
Can a phone image approve silicone tableware color tolerance?
No phone image can preserve the entire chain of lighting, white balance, exposure, compression and display calibration. Photographs can document gross differences and defects, but final approval should refer to physical samples and defined measurements.
For remote projects, both parties can standardize photography and courier approved samples. The release record should still identify the physical or numerical master rather than a screenshot in a chat history.
Translate Visual Expectations into Measured Evidence
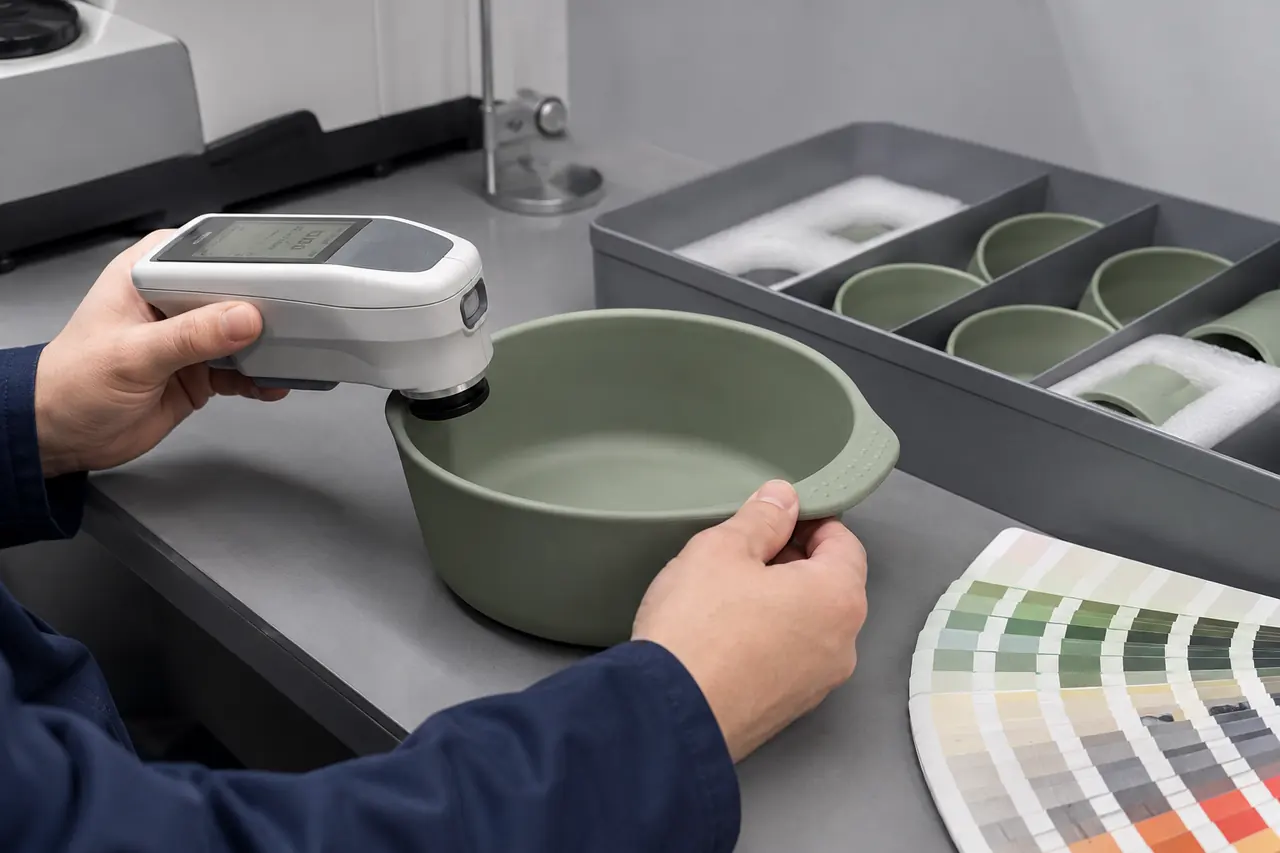
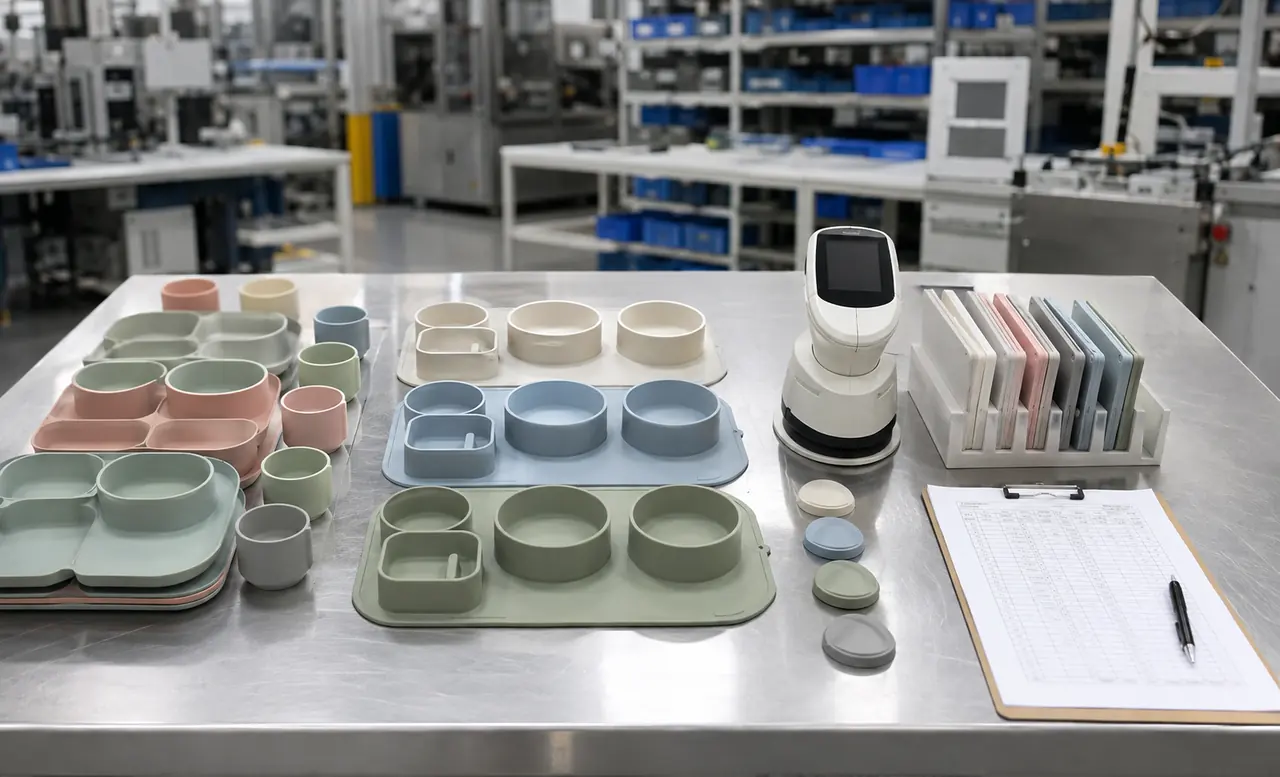
A spectrophotometer or colorimeter provides repeatable coordinates when settings are controlled. Instrument geometry, illuminant, observer, aperture, surface position and color-difference formula must be recorded so later results remain comparable.
Measurement locations should avoid gates, strong curvature or textured zones unless those areas are specifically part of the acceptance method. A small aperture can exaggerate local effects, while a large aperture may average away a buyer-visible problem.
Measure several pieces and relevant cavities instead of reporting one favorable sample. Review the distribution and direction of results because an average can conceal a subgroup that is consistently too dark, too yellow or too glossy.
Numerical evidence should support visual judgment rather than replace it. Texture, translucency, local streaks and assembled-set appearance can remain commercially important even when a calculated difference passes.
How should buyers establish a measured silicone color limit?
Use production-intent trials to identify what difference remains visually acceptable on the real component. The final limit should reflect buyer risk and demonstrated process capability instead of an arbitrary number copied from another supplier.
Document the chosen formula and conditions beside the limit. A delta value without its method is incomplete because different formulas and settings can produce different results from the same pair of samples.
Use Boundary Samples to Prevent Subjective Rejection
A single approved center sample shows the target but does not show the edge of acceptance. Light, dark and hue-shift boundary samples make the commercial decision easier for inspectors, factories and remote buyer teams.
Boundary samples must be prepared from the released material construction and real tool surface. Flat chips can support formulation work, but they do not fully represent thick walls, suction bases, ribs or polished and matte areas.
Store references away from heat, sunlight, dust and chemicals that may change appearance. Working samples should be replaced under a documented schedule while the protected master remains the authority.
A sample library needs revision control. When a buyer approves a new color, material or surface, obsolete standards should be marked clearly so they cannot be used for later inspection.
When color changes require a new approval cycle
Changes to silicone grade, pigment supplier, dosage, surface texture, tool, cure conditions or product geometry may alter appearance. The change review should decide whether new visual samples, measurement data or compliance evidence are required.
For projects involving new cavities or surfaces, our custom mold and tooling process links drawing approval, trial parts and production release. Color decisions should use the same controlled revision path.
Control Silicone Color across Lots Cavities and Shifts
Bulk production begins with released material and pigment identities, verified weighing and a documented mixing route. Operators should not correct shade through informal pigment additions because the change affects repeatability and may alter the approved material basis.
First-piece inspection should occur after the process stabilizes. Start-up material, purge history and changing mold temperature can produce samples that do not represent normal production conditions.
Where multiple cavities, machines, shifts or compound lots contribute to one shipment, the sampling plan should cover each relevant source. A cavity map and time-based records reveal patterns that one convenient sample cannot show.
Final inspection should include assembled sets and packaging presentation. Components may individually meet limits but still look inconsistent when items from opposite tolerance boundaries are packed together.
What evidence supports silicone tableware color tolerance at shipment
The release file should identify the valid standard, measurement setup, sample count, lot and cavity coverage, results, visual review and disposition of any deviation. Retained samples should trace to the same production and packing records.
If results move toward a limit, hold the affected material and verify the measurement system before changing the process. Correction should be demonstrated across normal production duration, not through one favorable piece.
Write a Color RFQ That Suppliers Can Quote Consistently
State the product revision, component list, material direction, color references, quantity split, target market and sales channel. Suppliers cannot quote the same control plan when one assumes a generic stock color and another assumes a tightly matched custom collection.
Ask how many color trials are included, which sample controls production and how repeat orders are compared. The response should describe approval points and records rather than promise an exact match before trials exist.
Define viewing lights, measurement settings, locations, sample count and set-matching expectations. If a new product has no capability data, allow the final numerical limit to be confirmed from approved trial evidence.
Commercial variables such as sample charges, MOQ, lead time and testing depend on final formulation, component count, color split and packaging. Record them in the project quotation instead of assuming one listing applies to every configuration.
Prepare evidence for a factory color review
Use the Naike Group project inquiry form to share your drawings, physical reference, required colors, quantities and market. Our factory can identify missing approval conditions before sampling starts.
Review our factory capability page to understand how development, molding and quality checkpoints connect. A useful color quotation depends on an executable control path, not only a target shade.
Silicone Color Evidence: Useful versus Incomplete
This comparison helps buyers distinguish a repeatable approval record from evidence that looks precise but cannot control production. Record the selected comparison assumptions in the silicone tableware color tolerance project brief before quotation.
| Evidence | Useful When | Limitation | Buyer Decision | Factory Record |
|---|---|---|---|---|
| Pantone or brand swatch | Communicating initial direction | Paper and silicone differ | Request molded trials | Reference identity and revision |
| Phone photograph | Recording gross visible concerns | Uncontrolled camera and display | Do not use as sole approval | Controlled photo plus sample ID |
| Center physical sample | Showing the intended target | Does not define acceptance edges | Add boundary samples | Signed retained master |
| Instrument reading | Comparing results under fixed settings | Can miss texture and local defects | Pair with visual inspection | Settings locations and dataset |
| Assembled retail set | Evaluating component coordination | May not explain the root cause | Apply set-matching rule | Packing and component lot record |
| One production piece | Initial troubleshooting only | Cannot represent cavities or time | Expand the sampling plan | Lot cavity shift coverage |
B2B Buyer Checklist for Silicone Color Approval
Use this checklist before signing a sample or releasing a repeat order. Every answer should identify the current project revision and evidence owner. Record every answer against the current silicone tableware color tolerance project assumptions and approval owner.
| Check | Question | Why It Matters |
|---|---|---|
| Product construction | Are silicone grade opacity surface and geometry fixed? | Appearance changes when the underlying construction changes. |
| Target reference | Which physical sample or dataset is the controlling master? | Digital files alone cannot preserve a repeatable color decision. |
| Viewing conditions | Which daylight retail and warehouse lights are relevant? | A match under one light may separate under another. |
| Instrument setup | Are geometry illuminant observer aperture and formula recorded? | Results are not comparable when settings change. |
| Sampling coverage | How many pieces cavities lots and shifts will be checked? | One piece cannot represent the full shipment. |
| Boundary standards | Do light dark and hue limits have physical examples? | Boundary samples reduce subjective rejection. |
| Set coordination | Must all components match as one retail collection? | Individually passing parts may still look inconsistent together. |
| Defect separation | Are streaks contamination and gloss differences controlled separately? | A numerical average can hide buyer-visible defects. |
| Revision triggers | Which approved construction changes require the color file to be released again? | Previous evidence may not represent a revised material or process. |
| Repeat-order record | Can current results trace to the approved reference and production lots? | Traceability supports focused correction and reliable repeats. |
Factory Control Notes for silicone tableware color tolerance
These checkpoints turn a subjective visual preference into a shared buyer and factory release system. Each silicone tableware color tolerance decision should identify its owner, evidence and release condition.
1. Product construction control for silicone tableware color tolerance
For silicone tableware color tolerance, the product construction checkpoint must become a dated project record rather than an informal chat instruction. The resulting product construction record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Are silicone grade opacity surface and geometry fixed?”
Appearance changes when the underlying construction changes. For the product construction decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
2. Target reference control for silicone tableware color tolerance
For silicone tableware color tolerance, the target reference checkpoint must become a dated project record rather than an informal chat instruction. The resulting target reference record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Which physical sample or dataset is the controlling master?”
Digital files alone cannot preserve a repeatable color decision. For the target reference decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
3. Viewing conditions control for silicone tableware color tolerance
For silicone tableware color tolerance, the viewing conditions checkpoint must become a dated project record rather than an informal chat instruction. The resulting viewing conditions record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Which daylight retail and warehouse lights are relevant?”
A match under one light may separate under another. For the viewing conditions decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
4. Instrument setup control for silicone tableware color tolerance
For silicone tableware color tolerance, the instrument setup checkpoint must become a dated project record rather than an informal chat instruction. The resulting instrument setup record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Are geometry illuminant observer aperture and formula recorded?”
Results are not comparable when settings change. For the instrument setup decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
5. Sampling coverage control for silicone tableware color tolerance
For silicone tableware color tolerance, the sampling coverage checkpoint must become a dated project record rather than an informal chat instruction. The resulting sampling coverage record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “How many pieces cavities lots and shifts will be checked?”
One piece cannot represent the full shipment. For the sampling coverage decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
6. Boundary standards control for silicone tableware color tolerance
For silicone tableware color tolerance, the boundary standards checkpoint must become a dated project record rather than an informal chat instruction. The resulting boundary standards record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Do light dark and hue limits have physical examples?”
Boundary samples reduce subjective rejection. For the boundary standards decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
7. Set coordination control for silicone tableware color tolerance
For silicone tableware color tolerance, the set coordination checkpoint must become a dated project record rather than an informal chat instruction. The resulting set coordination record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Must all components match as one retail collection?”
Individually passing parts may still look inconsistent together. For the set coordination decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
8. Defect separation control for silicone tableware color tolerance
For silicone tableware color tolerance, the defect separation checkpoint must become a dated project record rather than an informal chat instruction. The resulting defect separation record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Are streaks contamination and gloss differences controlled separately?”
A numerical average can hide buyer-visible defects. For the defect separation decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
9. Revision triggers control for silicone tableware color tolerance
For silicone tableware color tolerance, the revision triggers checkpoint must become a dated project record rather than an informal chat instruction. The resulting revision triggers record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Which approved construction changes require the color file to be released again?”
Previous evidence may not represent a revised material or process. For the revision triggers decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
10. Repeat-order record control for silicone tableware color tolerance
For silicone tableware color tolerance, the repeat-order record checkpoint must become a dated project record rather than an informal chat instruction. The resulting repeat-order record record must name its owner, source evidence, revision authority and the commercial consequence of a late change after the buyer asks, “Can current results trace to the approved reference and production lots?”
Traceability supports focused correction and reliable repeats. For the repeat-order record decision in this silicone tableware color tolerance project, our factory links the checkpoint to the quotation, approved sample, purchase order or inspection standard that governs the next approval. If the silicone tableware color tolerance evidence is incomplete, the team holds that approval gate, closes the information gap and records the revised assumption before production continues.
Authoritative References and Practical Limits
ISO/CIE 11664-4 defines the CIE 1976 L*a*b* colour space used in instrumental color communication. Review the official ISO standard overview. Buyers should confirm how this reference applies to the named product, target market and current silicone tableware color tolerance project.
ASTM Committee E12 identifies D2244 as its practice for calculating color tolerances and differences from instrumentally measured coordinates. Review the official ASTM E12 fact sheet. Buyers should confirm how this reference applies to the named product, target market and current silicone tableware color tolerance project.
The U.S. FDA explains the regulatory framework for colorants used in food-contact polymers. Review the official FDA colorant guidance with qualified compliance support. Buyers should confirm how this reference applies to the named product, target market and current silicone tableware color tolerance project.
This guide explains a factory approval method and does not prescribe a universal tolerance, certification or legal conclusion. The buyer must approve the actual product, formulation, intended use and target-market requirements with qualified technical and compliance professionals.
Silicone Tableware Color Tolerance FAQ
Can a Pantone code be the final silicone color standard?
It is usually a direction rather than the complete production standard. Buyers should approve a molded physical sample made with the actual material, geometry and surface.
What color difference number should a buyer specify?
There is no universal number for every product. Establish the limit from visual risk, real trial parts, defined measurement settings and demonstrated process capability.
Why do matching parts look different in photographs?
Lighting, automatic white balance, exposure, compression and display calibration alter appearance. Use photographs as supporting records rather than the sole approval authority.
Should every component in a feeding set use one tolerance?
Not automatically. Geometry, thickness and surface can change appearance, so component limits and a final set-matching rule may both be needed.
When should a repeat order be reapproved?
Review approval when silicone, pigment, tool, surface, geometry, process or intended use changes, or when the retained standard is no longer reliable. The change record should identify which evidence must be renewed.
What should be included in a color RFQ?
Provide the product revision, component list, material direction, physical reference, colors, quantity split, market, packaging and required inspection evidence. Name the approval owner and the reference that will govern bulk production.
Conclusion: Approve Color as Evidence Not a Promise
A reliable silicone tableware color tolerance links the real product construction to a physical master, controlled lighting, defined measurements, representative sampling and change control. That system lets purchasing and quality teams distinguish normal variation from a correctable process shift.
Our factory records color decisions through development trials, retained samples, cavity and lot checks, and documented release conditions. The goal is not an unsupported claim of perfect sameness but a repeatable standard that protects the buyer collection.
When your target shades and component plan are ready, request a silicone color approval review. Naike Group manufacturing team will identify the references and evidence needed for a meaningful quotation.
Set the Color Approval Path before Sampling
Share the product revision, physical color reference, component list, quantities and target market for a factory-side review. Our manufacturing team will use those details to define the next review step for your silicone tableware color tolerance project.
Request a Custom Quote
Share your product, quantity, target market and customization needs. Our factory team will reply with the next practical step.
Continue Your Sourcing Research
The six newest factory-side articles are updated automatically by publication date.
Wheat Straw vs Bagasse Tableware: Buyer Comparison
A B2B decision guide comparing reusable wheat-straw polypropylene composite tableware with molded bagasse fiber formats across use, evidence, operations and end of life.
Can Wheat Straw Tableware Be Recycled? Buyer Q&A
A practical buyer answer on whether reusable wheat-straw composite tableware can enter PP recycling streams, which evidence matters, and how to qualify market claims.
Global SKU vs Regional SKU: Tableware Decision Guide
A buyer decision framework for choosing one global tableware SKU or controlled regional variants across compliance, packaging, logistics, inventory and change control.
Australia Food Packaging Evidence: Buyer Guide
A practical evidence guide for Australian food-packaging buyers covering intended use, migration risk, supplier assurance, testing, hygiene, release and change control.
EU PPWR Tableware Packaging vs Conventional Packs
A buyer comparison of PPWR-ready and conventional tableware packaging across product protection, material choices, empty space, evidence, labeling and release timing.
Prop 65 Tableware Requirements: Buyer Q&A
A practical buyer Q&A for defining California Proposition 65 exposure scenarios, evidence, warning decisions, supplier records and release controls for tableware.