Barcode Label Verification: Evidence Guide
Prevent retail and logistics failures by linking every approved barcode and label to controlled data, measurable print-quality evidence, physical placement checks, and the released production lot.
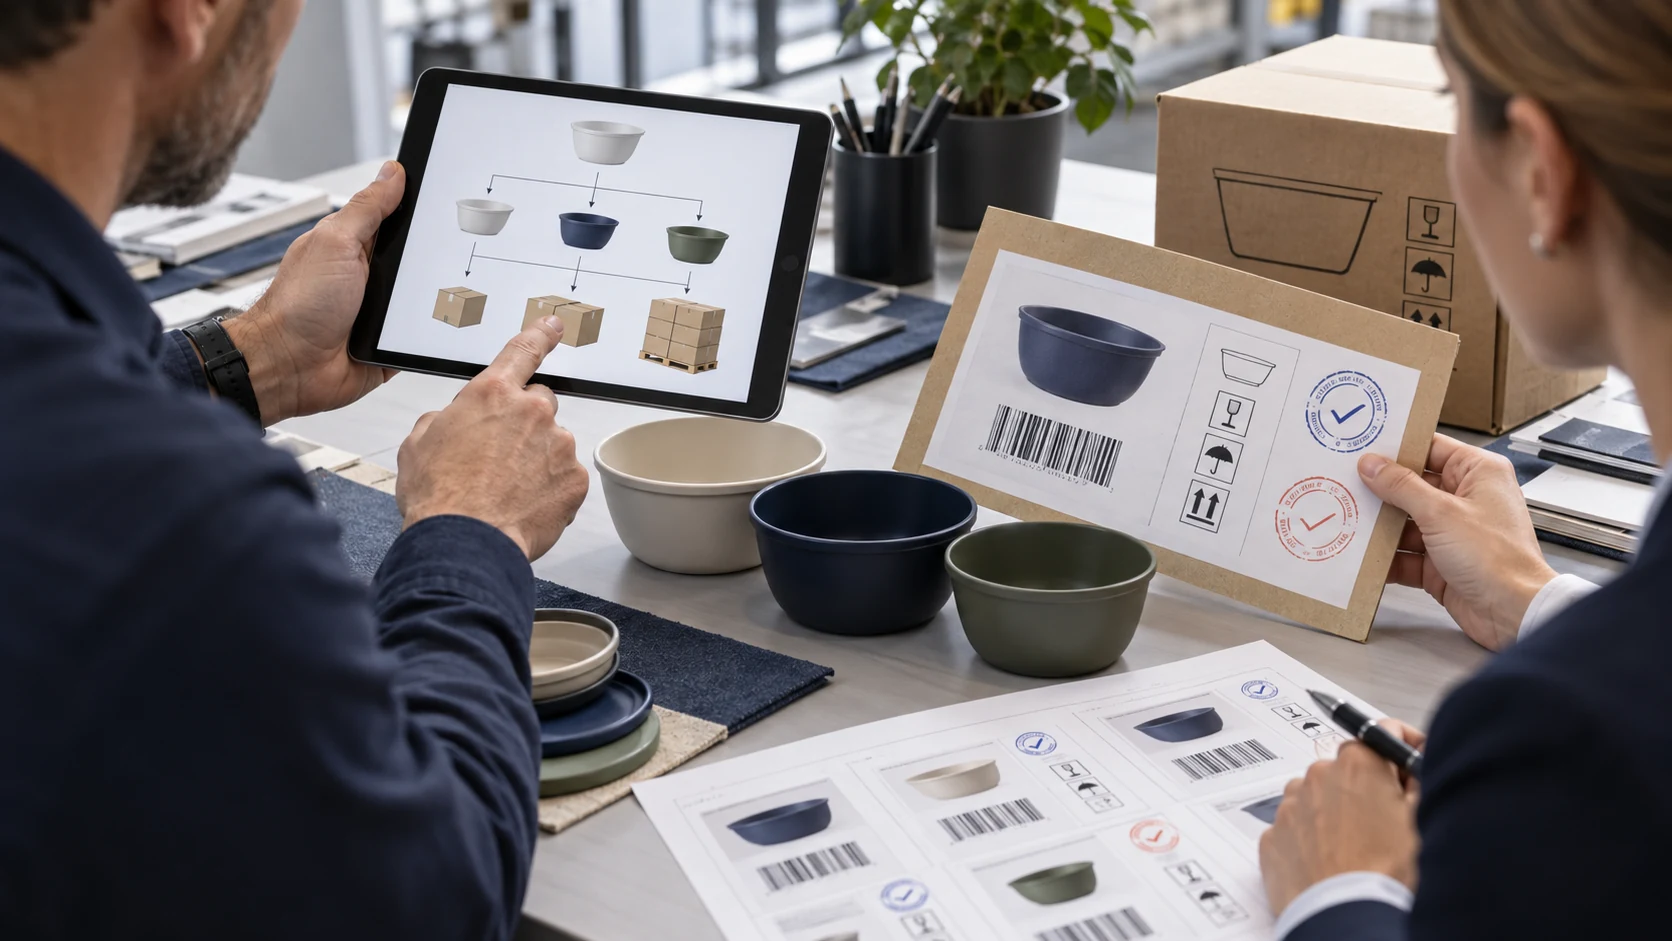
The evidence that best prevents barcode and label errors is a linked approval pack: an authorized GTIN-to-SKU master, a decoded artwork proof, a standards-based print-quality report from the final substrate, an approved placement sample, and production records that tie the released label version to the packed lot. This barcode label verification chain catches both symbol defects and the more costly error of placing a perfectly readable but incorrect label on a shipment.
A successful scan is not enough evidence. It confirms that one reader decoded one symbol under one condition, but it may not prove the encoded number belongs to the correct trade item, the symbol meets the required application specification, the quiet zones and dimensions are acceptable, the label is in the right location, or the production line used the approved revision.
B2B buyers should therefore approve the identification system rather than a PDF in isolation. The system connects commercial master data, artwork, physical packaging, print process, inspection method, line controls, change history, and shipment release so that every participant is checking the same identity.
Buyer Answer: What Barcode Evidence Should Be Required?
Require five connected records before shipment: the buyer-approved item and GTIN master, a proof showing decoded data and human-readable interpretation, a verification report for production-representative labels, a signed placement and legibility sample, and a lot-specific packing record. Each record should show the SKU, label revision, date, responsible approver, and acceptance basis so evidence cannot be borrowed from another product.
Add line clearance, first-off checks, periodic in-process checks, and retained samples when several SKUs or regional label versions share one packing area. The practical goal is not paperwork volume; it is a traceable answer to four questions: Is the data correct, is the symbol measurable, is the label usable on the finished pack, and was that exact version applied to the correct goods?
Build an Authorized GTIN-to-SKU Master Before Artwork
The first control is ownership of the identification data. Procurement should issue or approve a master that maps each sellable unit, inner pack, and logistics unit to its product name, variant, quantity, destination, GTIN or other identifier, barcode symbology, and responsible data owner. A printer should never invent a number, copy one from an earlier SKU, or infer carton hierarchy from an email thread.
The master should distinguish consumer units from cases and pallets because each level may require different identifiers and symbols. A bowl set sold at retail is not automatically the same trade item as a master carton containing twelve sets, even when both descriptions sound similar. Mixing packaging levels can create a barcode that scans cleanly but returns the wrong quantity or item record downstream.
Treat human-readable text as controlled data rather than decoration. The digits printed beneath a symbol, product name, pack count, color, size, country-of-origin statement, handling text, and destination-specific fields should all reconcile to the same released SKU. When the text and encoded data disagree, the buyer needs an explicit rule for which source stops production and who resolves the discrepancy.
Version control begins with unique filenames and a revision register. Each artwork should show the SKU, revision, approval date, and status, while superseded files are moved out of production access rather than merely renamed old. If a buyer changes a GTIN, pack count, legal line, or destination label, the change record should identify affected work orders and inventory already printed.
Ask for a decoded-data proof, not only a visual image. The proof should list the symbology detected, decoded string, check digit result where applicable, and comparison to the approved master. A reviewer can then catch a transposed digit or unintended character even when the bars look visually plausible.
Projects with many regional variants benefit from a controlled matrix that shows which labels may coexist and which combinations are prohibited. Buyers can send the SKU and packaging hierarchy for an identification review before releasing artwork, while final number allocation and retailer registration remain the responsibility of the authorized data owner.
Barcode label verification starts with identity, not print contrast
A technically excellent symbol can still cause rejection if it identifies the wrong trade item. The approval chain must therefore lock the number, packaging level, product description, destination, and artwork revision before judging print quality.
The custom solutions process can organize product and packaging inputs for private-label development. It does not replace the buyer, retailer, or GS1 licensee as the authority for identifier assignment and market data.
Approve a Decoded Artwork Proof Before Printing Plates
Artwork review should separate content from appearance. First confirm every encoded and printed field against the authorized master, then evaluate symbol construction, size, quiet zones, colors, orientation, and surrounding graphics. This order prevents a visually polished layout from distracting reviewers from an incorrect number or packaging level.
The proof should state the target symbol type and application environment. Retail point-of-sale, warehouse scanning, logistics labels, and two-dimensional applications can have different requirements, so a generic instruction to add a barcode is incomplete. The responsible party should name the applicable specification and the minimum acceptance level expected by the customer or channel.
Do not resize a barcode by dragging one edge in design software. Distortion can change module width, bar relationships, or aspect ratio, and reducing height can weaken omnidirectional scanning even when the number still decodes on a phone. The released proof should state intended dimensions and prohibit uncontrolled scaling or recreation.
Quiet zones need protected space around the symbol. Borders, patterns, folds, seams, tape, windows, icons, and nearby text can intrude into this area or create competing contrast. The artwork approval should include a measurement from the final die line, not a judgment that the surrounding area looks white enough on screen.
Color approval must consider the scanner light and the final material. Dark bars on a light background are generally robust, while certain visually contrasting color pairs may offer poor scanner contrast; transparency, metallic effects, gloss, fiber texture, and show-through can add risk. A digital color proof cannot demonstrate final reflectance or print behavior.
Generate the symbol from controlled data with traceable software settings, then lock the output as part of the approved artwork package. Record who generated it, which data source was used, the artwork revision, and any bar-width compensation supplied by the printer. These details make later investigation faster than comparing screenshots.
The artwork proof should expose every decision a printer could otherwise guess
A useful proof identifies the data source, symbology, dimensions, position, colors, substrate, orientation, and revision. If any of those fields remain implicit, two competent suppliers can produce different labels from the same email attachment.
For pack development, the custom tableware product overview helps buyers frame product, carton, insert, and label choices. The final barcode specification still needs its own controlled approval and channel-specific acceptance basis.
Verify Print Quality on the Final Label and Substrate
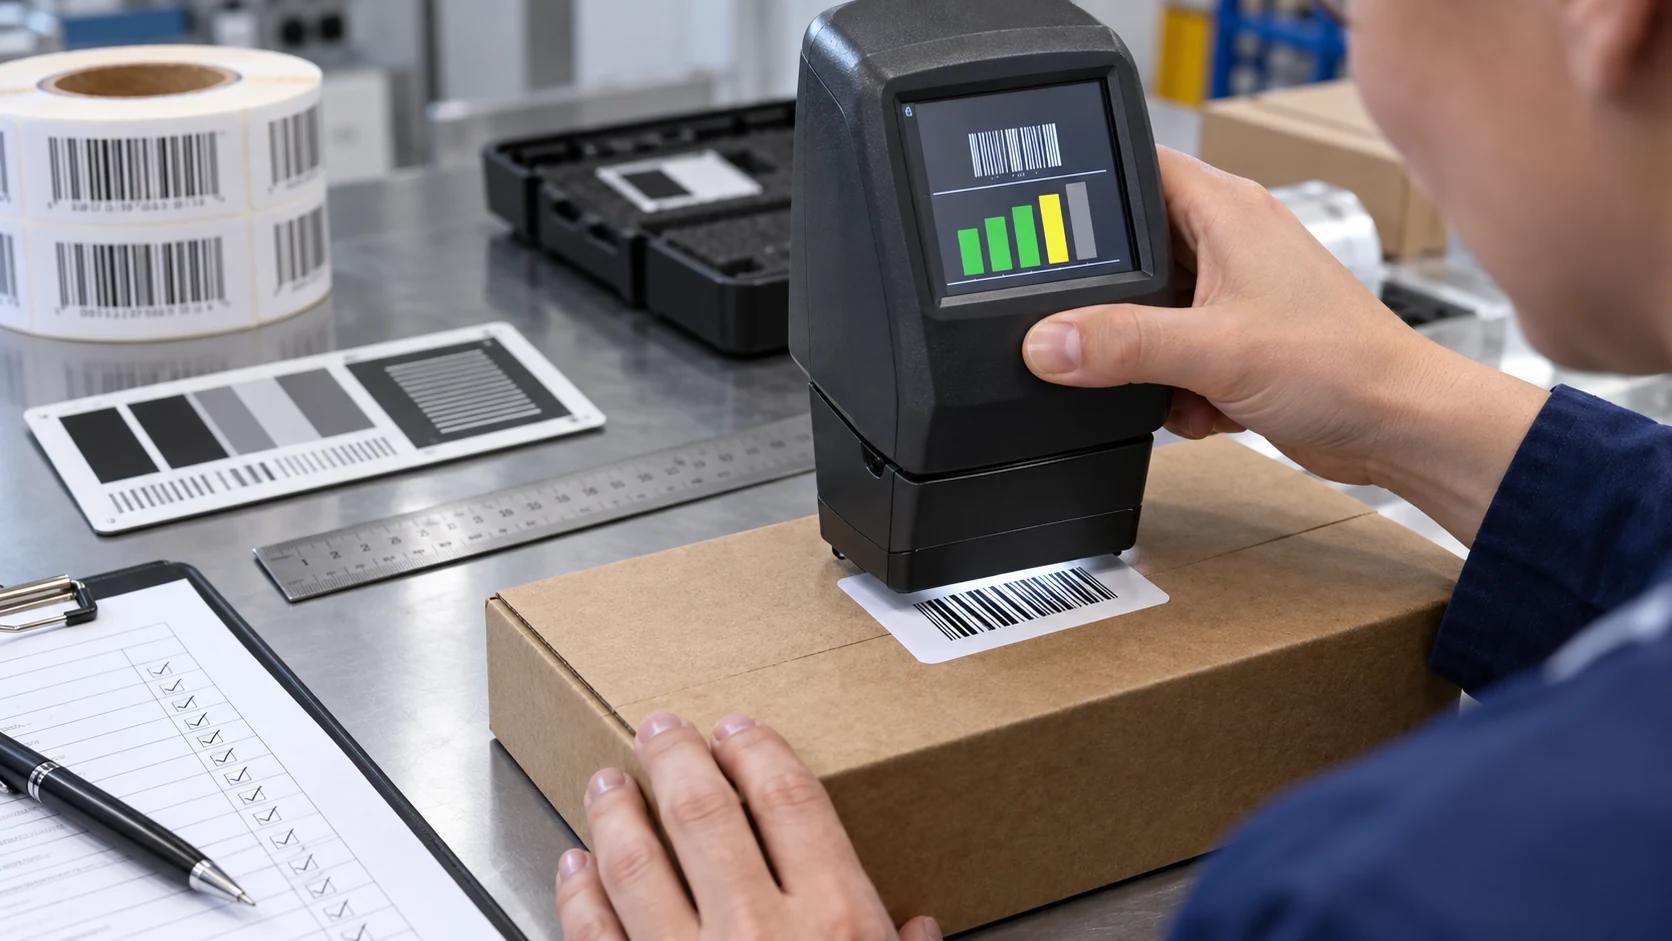
Print-quality verification measures characteristics of a produced symbol under defined conditions and reports an overall grade or result against an identified specification. That is different from opening a camera app or pulling a carton past one warehouse scanner. A verifier can reveal contrast, modulation, defects, decodability, dimensional, or quiet-zone problems that casual scanning does not quantify.
The report should identify the tested item and not merely attach a grade. Include product or SKU, barcode type, decoded data, print method, final substrate, symbol specification table or application basis, verifier make and model, software version, calibration status, aperture, light source, measurement date, operator, and sample location. Without that context, a number such as 3.0 cannot be interpreted or reproduced reliably.
Test production-representative material in its final configuration whenever practical. A thermal-transfer label verified flat on its release liner may perform differently after application over corrugated flutes, around a curve, beneath film, near a carton edge, or after rubbing during transport. The evidence should represent the surface and presentation in which the symbol will actually be scanned.
Sampling must reflect process risk. A single excellent preproduction sample does not establish stability across print heads, ribbon lots, ink batches, plates, shifts, carton suppliers, or long production runs. Set first-off, periodic, after-adjustment, and final-lot checks according to volume and variation, then retain enough data to see a declining trend before symbols fail.
Separate verification from process monitoring. Online scanners or handheld readers can support one-hundred-percent readability checks or frequent alarms, while scheduled verifier measurements provide standardized diagnostic evidence. These controls complement each other because rapid scanning can catch gross failures and verification can characterize the underlying print-quality margin.
When a report fails, require corrective evidence rather than a replacement screenshot. The printer should identify the weak parameter, adjust substrate, ribbon, ink, pressure, speed, temperature, plate, artwork compensation, or maintenance as relevant, and then verify fresh samples. Rework labels should receive a new lot or revision link so failed stock cannot re-enter packing.
A scanner says decoded; a verifier explains measurable margin
Decoding is an operational result from a particular device and moment, while verification evaluates the symbol against specified measurement rules. Buyers should avoid using one as a substitute for the other when retailer or logistics acceptance depends on standardized quality.
The factory capability overview gives context for production and quality coordination. Actual verifier competence, calibration, sampling, and acceptance criteria should be documented for the individual project.
Confirm Placement, Legibility, and Label Durability on the Pack
A verified symbol can become unusable after it is placed on the product or carton. Curvature, flutes, seams, corners, closures, shrink film, straps, tape, handles, and stacked products can distort the symbol or block a reader. Approve a physical placement sample with dimensions from stable pack features rather than a floating box on an artwork PDF.
Placement evidence should include a straight-on image, contextual images of the full pack, measured offsets, label orientation, and the scanning direction expected in handling. For cylindrical or flexible packaging, inspect the worst curvature and deformation. For corrugated cartons, consider whether bars cross flute valleys and whether print or label pressure remains consistent.
Labels must remain attached and legible through the intended route. Adhesive selection, application temperature, dusty surfaces, silicone contamination, moisture, condensation, cold storage, abrasion, stretch wrap, and carton coatings can cause lift, flagging, wrinkling, or movement. Define conditioning and transport simulations that reflect the commercial claim instead of asking whether an adhesive is strong.
The complete label must be readable by people as well as equipment. Small fonts, low contrast, crowded translations, clipped characters, and ink spread can make product, lot, quantity, or origin fields ambiguous even when the barcode passes. The inspection standard should cover typography and critical text separately from symbol grade.
Check interaction with outer shipping marks and retailer labels. A carton may acquire carrier labels, pallet labels, compliance stickers, or warehouse routing marks after factory packing, and those additions can cover or compete with the intended symbol. Reserve application zones and, where necessary, provide diagrams to downstream logistics partners.
Preserve an approved physical standard or controlled high-resolution record that shows the final construction. The standard should identify substrate, adhesive, print method, finish, location, revision, and authorization. A loose label swatch is insufficient when placement and pack geometry are part of performance.
The finished pack is the evidence unit that matters
Verification on loose stock answers only part of the buyer question. A complete approval should show that the label remains scannable, readable, correctly located, and durable after the actual application and conditioning process.
For supplier and export preparation, the Naike Group company overview provides general manufacturing context. Destination rules, retailer manuals, and carrier requirements must still be checked against the live program.
Control Line Clearance and First-Off Packing Evidence
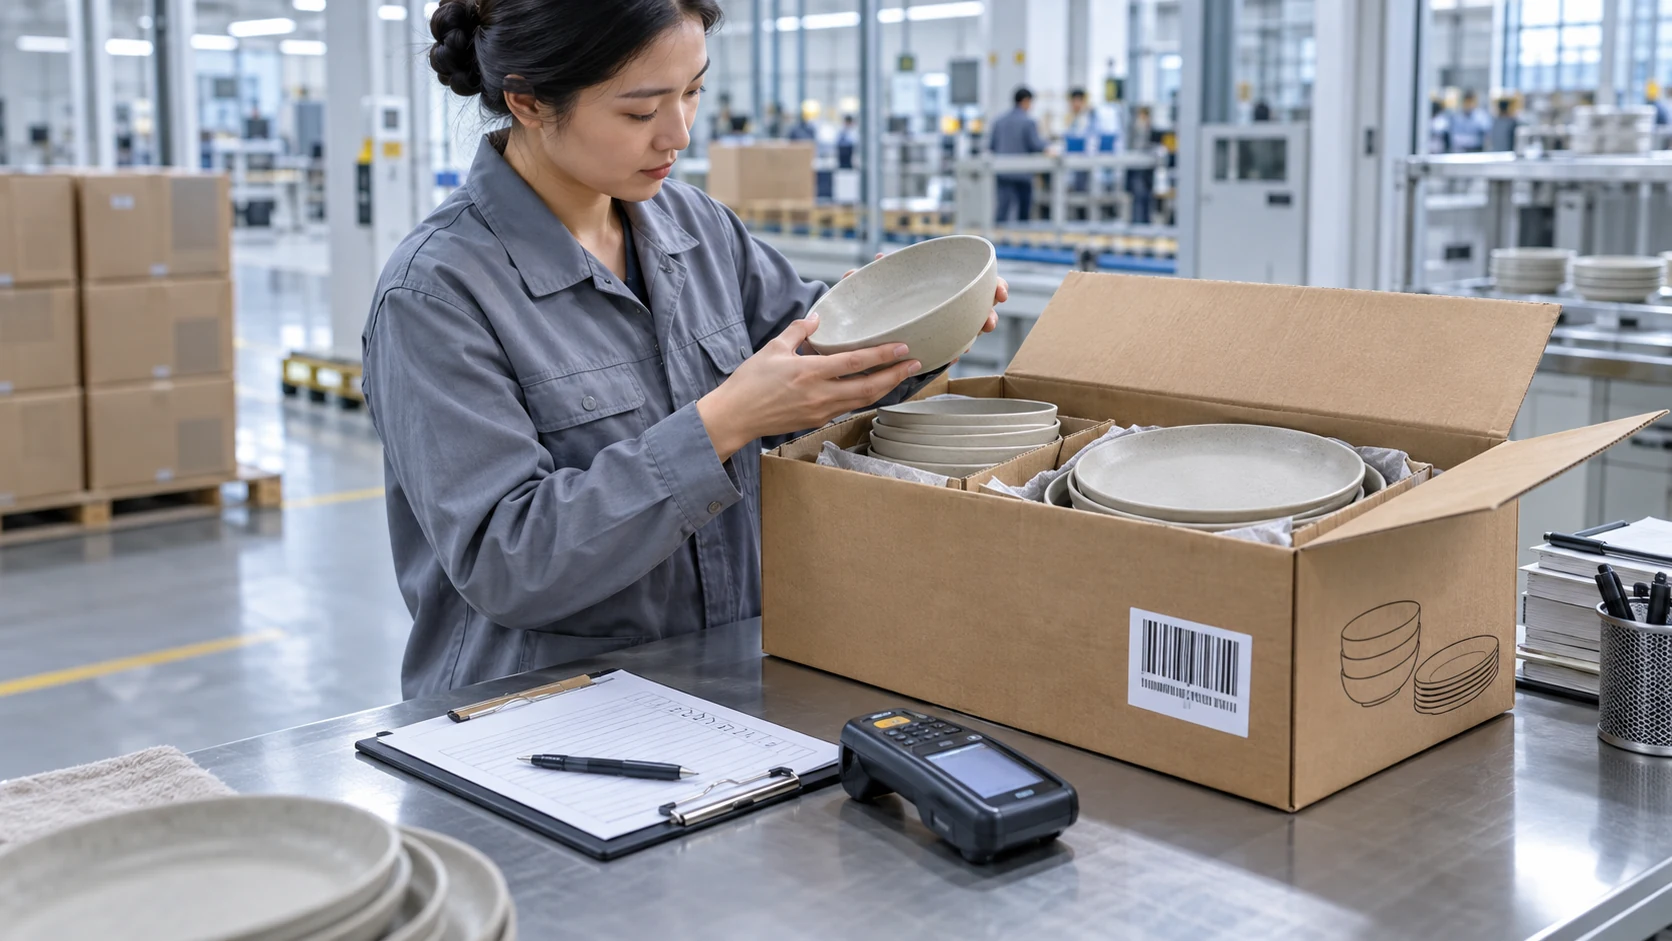
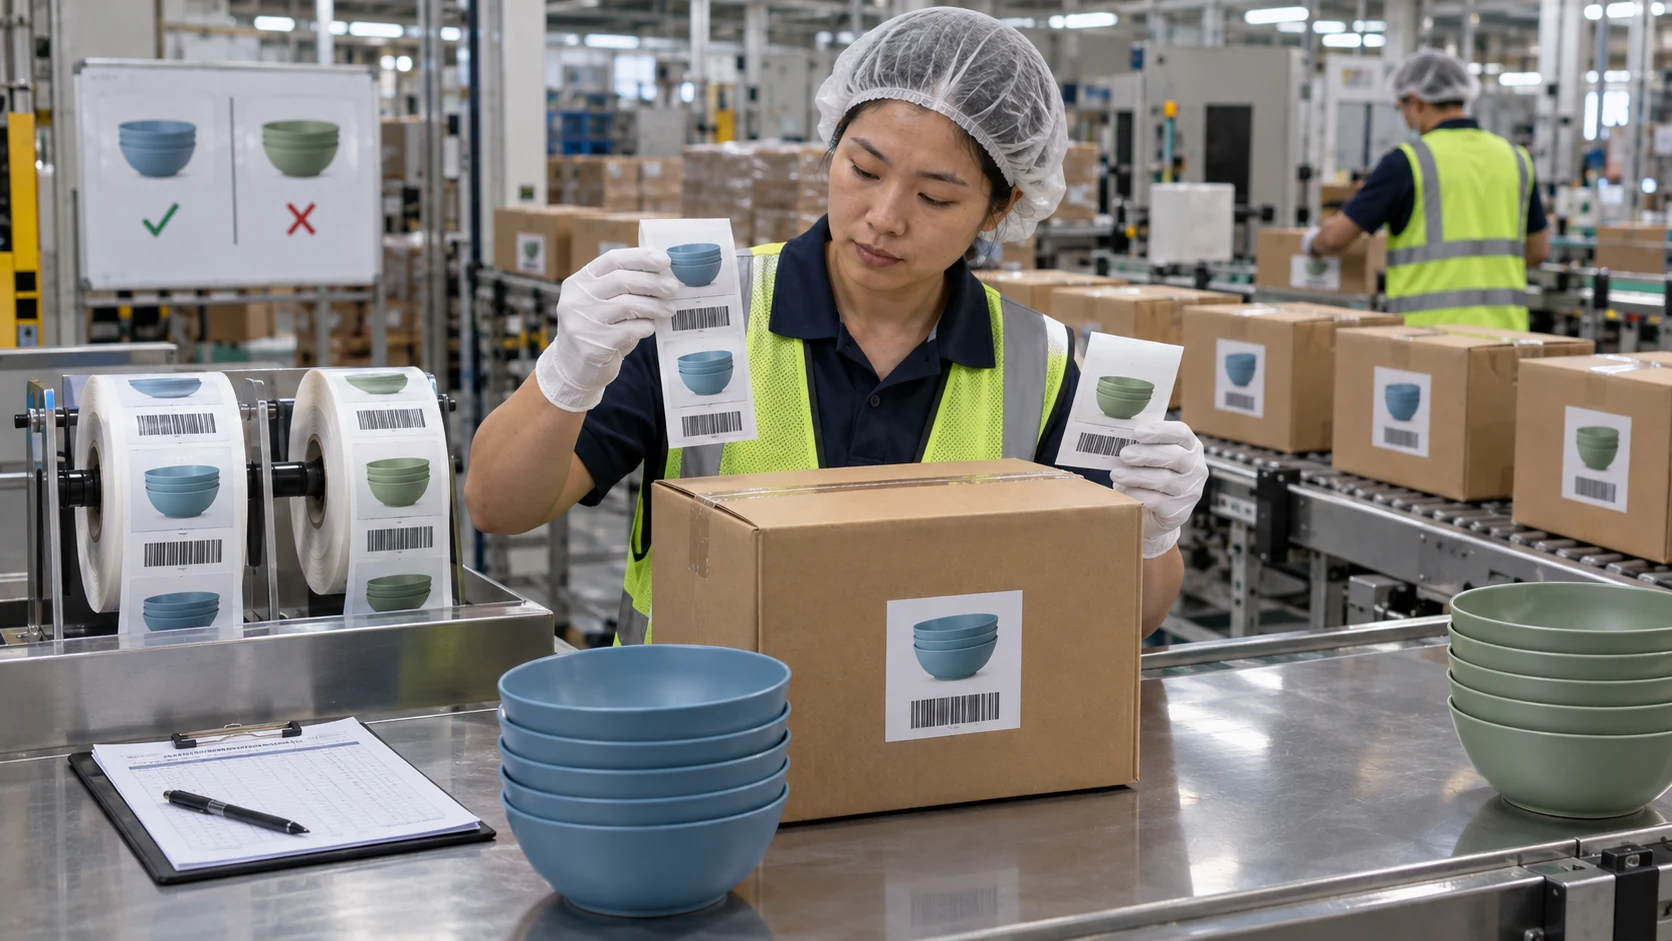
Many barcode failures are identity failures rather than print defects. A packing line may hold labels for several colors, set sizes, customers, languages, or destinations, and an operator can apply a readable label to the wrong goods. Line clearance removes obsolete and unrelated materials before a new work order begins and documents the result.
The work order should identify the only approved label revision and expected quantity. At changeover, reconcile labels issued, used, damaged, returned, and destroyed, and investigate unexplained differences. This simple accounting reduces the chance that leftovers remain near the line and appear in a later run.
First-off approval should compare the packed product, inner pack, master carton, and pallet information as a connected hierarchy. Inspect item identity, color, quantity, barcode data, readable text, label placement, carton marks, and any destination file before normal output continues. Photographs should show the full pack and close details while recording the order and timestamp.
Use two-person or electronic confirmation for high-consequence changes. One person can select and apply the label, while another checks decoded data and physical product against the controlled work order. If the same person performs both tasks, the procedure should add an independent release point before cartons leave the controlled area.
Periodic checks should be tied to real events, not only a clock. Recheck after roll changes, printer adjustments, power interruptions, maintenance, product changeovers, shift changes, and rework, because those events can alter either print quality or label identity. Record exceptions and disposition rather than converting every problem into a silent replacement label.
For multi-SKU projects, ask the factory to demonstrate its line-control logic during sample or pilot packing. Buyers can request a label-control and packing-evidence review with the SKU matrix, label variants, carton hierarchy, and retailer instructions attached.
Correct data must survive the production handoff
Artwork approval controls what should be printed, while line controls prove what was actually applied. Both are necessary when similar-looking products or destination labels share equipment, storage, or operators.
The factory capability overview offers general context for inspection planning. Project records should still define the label-specific sampling, responsibility, escalation, and release criteria.
Assemble Lot-Specific Release Evidence for Shipment
The release file should allow a buyer to trace a shipped carton back to the approved identification basis. Include the purchase order, SKU and pack hierarchy, artwork revision, label batch, print-quality results, first-off record, in-process checks, nonconformance disposition, retained sample reference, packing date, lot, and shipment authorization. Evidence from a different order or substrate should not be substituted because the title appears similar.
Create a concise evidence index rather than an unstructured folder of photographs. Each record should have an owner, date, version, acceptance result, and link to the affected lot. An index makes missing proof visible before loading and reduces the time needed to respond to a retailer query or receiving rejection.
Exceptions need documented boundaries. If a label roll is reprinted, a carton is relabeled, or a verification result is conditionally accepted, record the affected quantities, locations, authorization, reinspection, and segregation method. Vague notes such as fixed on line do not show whether all suspect goods were contained.
Retained samples should preserve the final configuration when risk justifies it. Keep a representative label on the actual carton or substrate, identify its lot and revision, and protect it from uncontrolled light, moisture, or abrasion that could confuse later evaluation. Digital images help retrieval but may not preserve adhesive, surface, reflectance, or construction evidence.
Use shipment release as the final reconciliation gate. Confirm the quantities by SKU, carton identifiers, pallet labels, destination marks, and documents all agree, then verify that no quarantined label or carton inventory was loaded. The release signature should point to evidence rather than relying on verbal confirmation from the packing floor.
After delivery, feed scan or receiving complaints back into the control plan. Capture the actual label, device or location, failure mode, shipment lot, and environmental condition before changing artwork or print settings. This prevents a local scanner issue, database mismatch, physical damage, and genuine print defect from being treated as the same root cause.
Release records turn barcode quality into shipment traceability
A complete file does not guarantee that every downstream database is correct, but it shows what the factory received, produced, checked, and released. That boundary is essential for assigning corrective action without guesswork.
Buyers should define record-retention periods and access in the purchase agreement. The period may depend on retailer programs, product lifecycle, warranty, legal obligations, and repeat-order cadence.
Barcode Evidence: What Each Record Proves
Use this matrix to prevent one form of evidence from being stretched beyond its purpose. Strong release decisions combine data, physical, measurement, and process records because no single document proves the entire identification system.
| Evidence record | What it proves | What it does not prove | Release use |
|---|---|---|---|
| GTIN-to-SKU master | Authorized identity and pack hierarchy | Print quality or application | Locks source data |
| Decoded artwork proof | Encoded string matches approved content | Final substrate performance | Releases artwork content |
| Verifier report | Measured symbol quality under stated conditions | Correct product-label pairing by itself | Accepts print process and sample |
| Placement sample | Location, orientation, context and accessibility | Long-run process stability | Approves pack configuration |
| Durability test | Performance after named conditioning or exposure | Universal performance in every route | Supports stated use claim |
| Line-clearance record | Wrong versions were removed at changeover | Symbol grade | Controls mixed-SKU risk |
| First-off inspection | Correct label is on the correct initial pack | Every later unit remains correct | Authorizes normal packing |
| Lot release file | Approved records link to shipped quantity | Retailer database accuracy | Supports shipment authorization |
B2B Buyer Barcode and Label Evidence Checklist
Complete all eight checks before shipment release. If an answer is missing, convert it into a named corrective action and hold point rather than accepting an assumption.
| Check | Question | Why It Matters |
|---|---|---|
| Identity master | Do GTIN, SKU, pack level, quantity and destination match? | Prevents readable symbols from identifying the wrong item. |
| Decoded proof | Was the encoded string independently compared with the master? | Finds digit and data-format errors before printing. |
| Specification | Are symbology, dimensions, quiet zones and acceptance basis named? | Stops design and printer guesswork. |
| Print report | Was final-substrate output measured with traceable verifier settings? | Provides reproducible quality evidence. |
| Physical placement | Is the symbol accessible, undistorted and away from seams or obstructions? | Protects real handling and scanning performance. |
| Line control | Were old labels cleared and issued quantities reconciled? | Reduces mixed-version and mixed-SKU application. |
| Lot traceability | Do first-off and periodic records identify order, label revision and lot? | Connects approval to shipped goods. |
| Release authority | Who resolves exceptions and authorizes shipment? | Prevents undocumented conditional acceptance. |
Official Sources for Barcode Quality and Label Control
These official sources help buyers define barcode production, verification, and marking questions. They do not allocate a GTIN, approve a finished label, certify a supplier, or replace the retailer and market requirements that apply to a specific shipment.
The GS1 General Specifications provide the core GS1 system rules and include barcode verification report fields such as decoded data, verifier details, calibration date, application basis, placement, and ISO/IEC print-quality grade. Buyers should use the current release and the symbol specification table that matches the actual scanning application.
The GS1 guidance on measuring printed barcode quality distinguishes standards-compliant verifier measurement from casual scanning and points users to the General Specifications for application-specific minimums and reporting. A supplier report should therefore identify its instrument, settings, calibration, sample, and specification rather than provide an unexplained grade.
The U.S. electronic Code of Federal Regulations, 19 CFR Part 134 publishes federal rules concerning country-of-origin marking for imported articles and containers. It is relevant context when an export label carries origin information, but buyers should obtain qualified advice for the exact product, container, exception, destination, and current interpretation.
Practical disclaimer: this guide is manufacturing and procurement information, not legal, regulatory, GS1 licensing, retailer onboarding, testing-laboratory, labeling, customs, or product-suitability advice. Buyers should confirm current identifier ownership, application standards, retailer manuals, destination rules, evidence scope, and finished-pack acceptance with the relevant authorities and qualified professionals.
Use a Layered Evidence Plan Instead of One Final Scan
Start with a data gate before graphic work: one controlled master for every product and packaging level, one owner for changes, and one independent decoded comparison. This is the cheapest point to stop a wrong GTIN because no plates, rolls, cartons, or finished packs need to be quarantined.
Add a preproduction gate on real materials. Verify representative print output, approve physical placement, and condition the label when adhesion, abrasion, moisture, curvature, film, or corrugated texture could change performance. Preserve the instrument context and acceptance basis with the result.
Build a production gate around line clearance and first-off approval. The operator should be able to show that only the released revision is available, that issued labels reconcile, and that the initial packed hierarchy matches the work order. Recheck after events that can change identity or print performance.
Finish with a shipment gate that indexes lot-specific records and exceptions. A buyer should be able to ask for one order and receive the relevant master revision, proof, measurement, placement, line, inspection, and release evidence without searching unrelated folders.
Scale the plan to consequence and complexity. A single stable SKU may need a compact file, while mixed colors, regional versions, retailer-specific labels, and shared packing lines need stronger reconciliation and sampling. More documents are not automatically better; stronger linkage is.
If downstream scans fail, investigate identity, database, print, placement, damage, and device conditions separately. A structured complaint sample and lot trail often prevent an unnecessary artwork change while exposing the real failure source.
Barcode Label Verification FAQ for B2B Buyers
Is a successful phone or handheld scan enough for approval?
No. It shows that one device decoded one sample under one condition, but it does not establish identifier ownership, application compliance, measurable print-quality margin, correct placement, or correct product pairing. Use scanning as a process check and standards-based verification as measurement evidence.
Should every label in a production run receive a verifier report?
Not necessarily, because verifier sampling and online readability monitoring serve different roles. Define first-off, periodic, event-triggered, and final sampling according to print method, run length, variability, customer requirements, and failure consequence.
What information should appear on a barcode verification report?
Include the tested SKU, symbology, decoded data, substrate, print method, application basis, verifier and software, calibration status, measurement settings, date, operator, results, placement assessment, and disposition. The report should link to the artwork revision and production lot when it supports shipment release.
How can buyers prevent two similar SKU labels from being mixed?
Use controlled storage, unique revision identifiers, line clearance, label issue reconciliation, first-off checks, and independent product-to-label confirmation. Segregate obsolete and quarantined stock so it cannot return to an active packing area.
When should barcode verification be repeated?
Repeat after material, artwork, printer, ribbon, ink, plate, size, substrate, supplier, or placement changes and after maintenance or adjustments that can affect output. Also sample during long runs and investigate trends before the minimum grade is crossed.
Make Barcode Label Verification a Shipment Evidence Chain
Effective barcode label verification does not end with a beep from a scanner. It links the authorized identity to decoded artwork, measured print output, final-pack placement, line controls, lot inspections, and shipment release so that both technical quality and product-label pairing are visible.
Buyers should demand evidence that is specific to the SKU, packaging level, substrate, revision, application, and production lot. That discipline prevents the most expensive ambiguity: discovering at receiving that nobody can prove whether the label, the database, the product, or the print process was wrong.
Set the evidence plan before artwork release and keep the hold points proportional to risk. The result is a repeatable identification system that supports procurement, factory quality, logistics, and corrective action across future orders.
Request a Barcode and Packing Evidence Review
Share the SKU hierarchy, GTIN master, artwork files, label materials, carton construction, retailer instructions, destination, quantities, and current acceptance criteria. Our manufacturing team can identify the proofs, samples, line controls, and release records needed for a production-ready quotation.
Request a Custom Quote
Share your product, quantity, target market and customization needs. Our factory team will reply with the next practical step.
Continue Your Sourcing Research
The six newest factory-side articles are updated automatically by publication date.
Wheat Straw vs Bagasse Tableware: Buyer Comparison
A B2B decision guide comparing reusable wheat-straw polypropylene composite tableware with molded bagasse fiber formats across use, evidence, operations and end of life.
Can Wheat Straw Tableware Be Recycled? Buyer Q&A
A practical buyer answer on whether reusable wheat-straw composite tableware can enter PP recycling streams, which evidence matters, and how to qualify market claims.
Global SKU vs Regional SKU: Tableware Decision Guide
A buyer decision framework for choosing one global tableware SKU or controlled regional variants across compliance, packaging, logistics, inventory and change control.
Australia Food Packaging Evidence: Buyer Guide
A practical evidence guide for Australian food-packaging buyers covering intended use, migration risk, supplier assurance, testing, hygiene, release and change control.
EU PPWR Tableware Packaging vs Conventional Packs
A buyer comparison of PPWR-ready and conventional tableware packaging across product protection, material choices, empty space, evidence, labeling and release timing.
Prop 65 Tableware Requirements: Buyer Q&A
A practical buyer Q&A for defining California Proposition 65 exposure scenarios, evidence, warning decisions, supplier records and release controls for tableware.